Home / Projects / Heavy Industrial & Mining / 1,200m Ultra-Long Aluminum Smelting Potline Complex in Bahrain: Millimeter-Precision PTA Crane Rail Alignment and Coastal Thermal-Slip Engineering
1,200m Ultra-Long Aluminum Smelting Potline Complex in Bahrain: Millimeter-Precision PTA Crane Rail Alignment and Coastal Thermal-Slip Engineering
Machined all heavy crane girder bearing seats on CNC floor-type milling centers, holding continuous track elevation and span tolerances within ± 1.0mm to completely prevent high-speed crane wheel wear and binding.
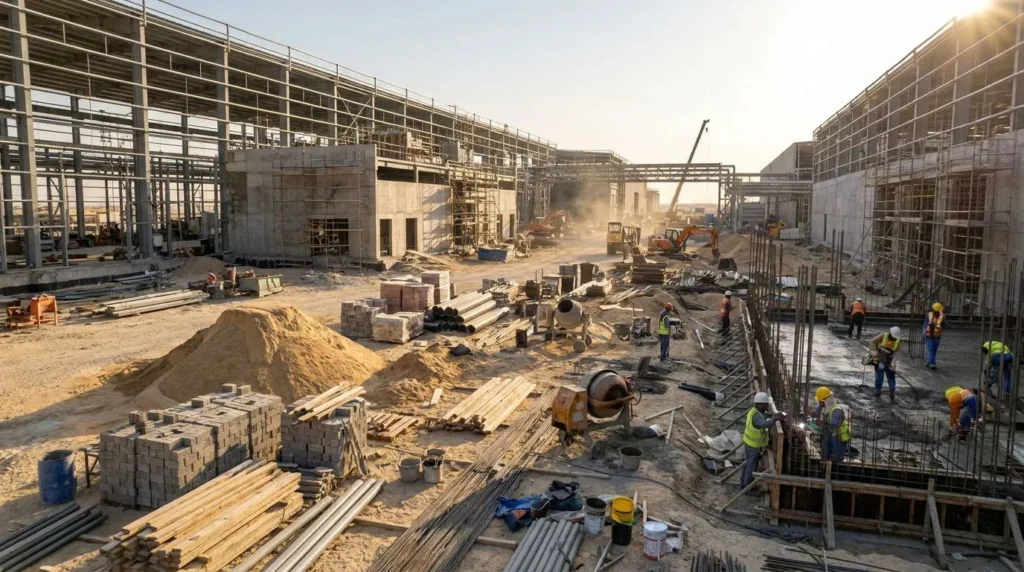
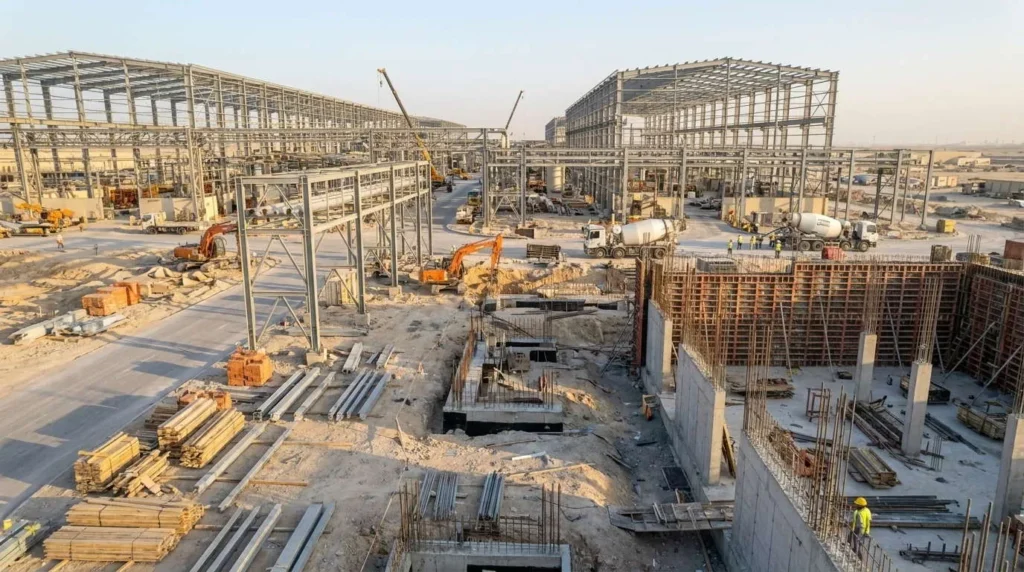
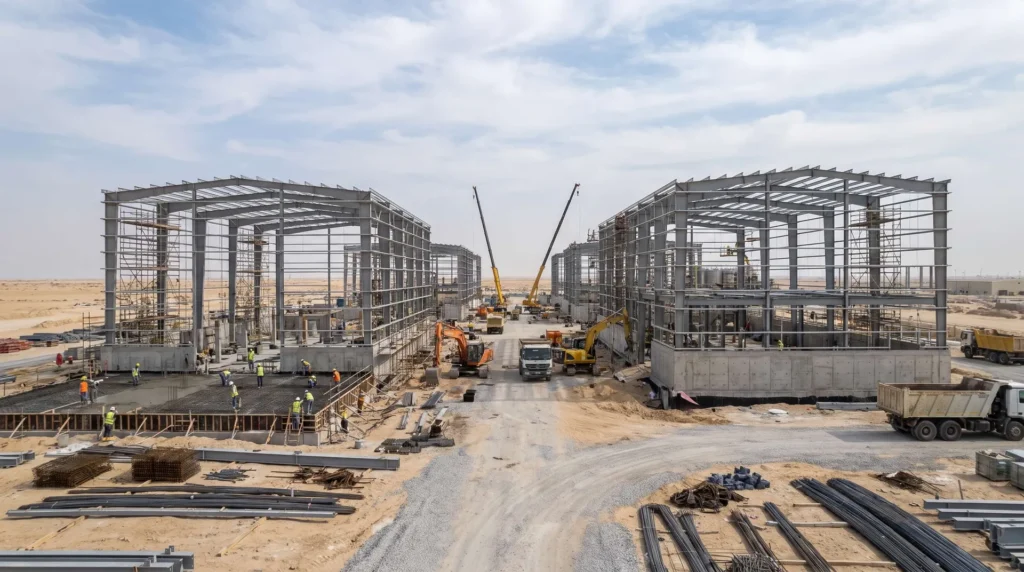
Project Overview
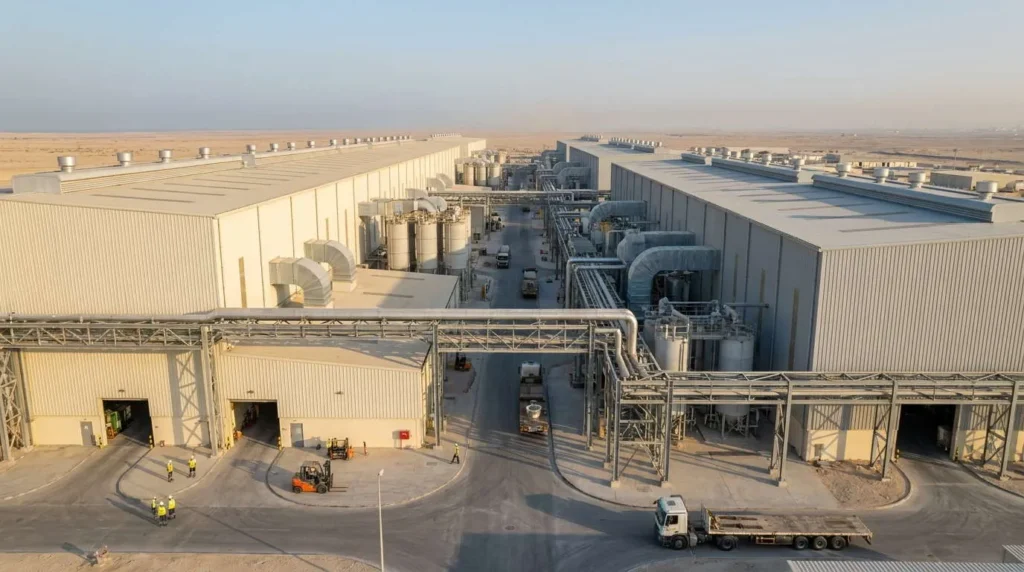
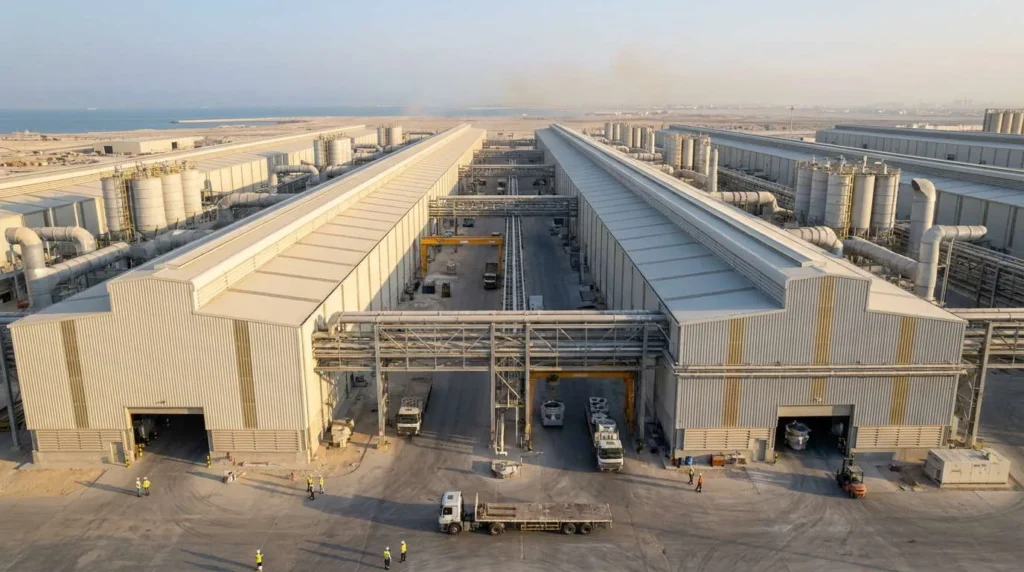
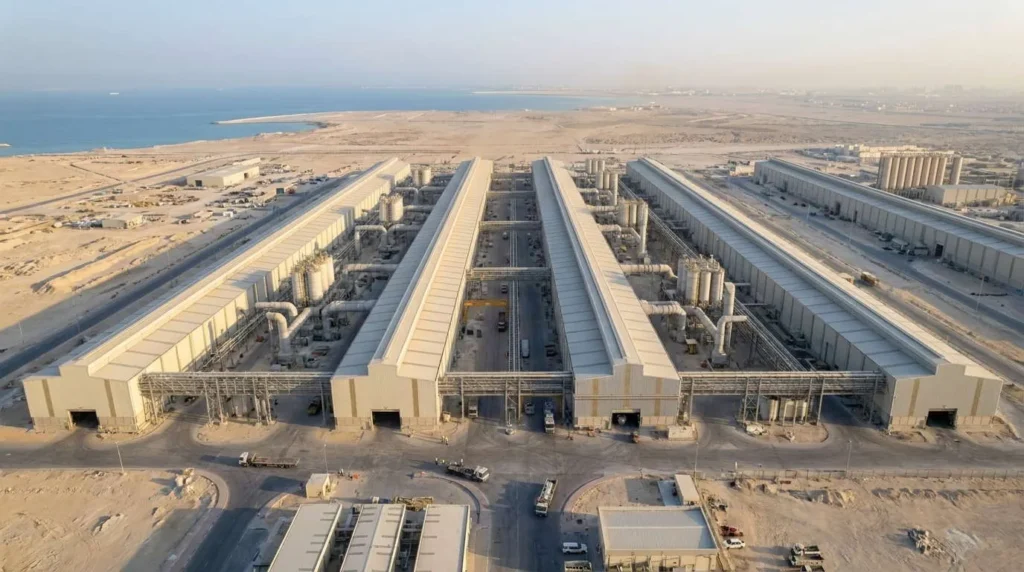
Constructing a world-scale aluminum smelting potline along the coastal desert of Bahrain is a high-stakes engineering endeavor. Spanning over 1.2 kilometers linearly, these twin potroom workshops house hundreds of reduction cells operating continuously at nearly 1,000°C, flanked by massive direct-current (DC) busbars carrying over 400 kA. For the EPC construction director, the primary operational fear was crane rail track misalignment and thermal expansion binding. Overhead Pot Tending Assemblies (PTAs)—massive, multimillion-dollar specialized cranes—must travel the entire 1,200-meter length around the clock to tap molten metal and replace carbon anodes. If the building’s heavy crane girders twisted by just 2 millimeters, or if thermal expansion joints jammed during Bahrain's blistering +50°C summer heatwaves, the PTA crane wheels would gnaw the rails or seize completely. Freezing an electrolytic pot due to an inoperable crane can ruin an entire potline, costing tens of millions of dollars.
Shijie Heavy Industry engineered a factory-integrated, slip-compensated structural steel system designed specifically for extreme desert-marine metallurgy. By modeling long-stroke thermal deformations across the 1.2km span, Shijie fabricated heavy welded H-columns, high-capacity box crane girders, and pre-adjusted temperature expansion joints with Teflon-slotted slide bearings. All crane-rail mounting holes and girder end-plates were milled on heavy-duty CNC floor borers, holding total span and straightness deviations strictly within ± 1.0 mm. Shipped in pre-sorted sequence lots matching crawler crane access corridors, over 26,000 tons of heavy steel were erected 100% bolted aloft without flame cutting or field reaming. The PTA cranes passed trial runs at full travel speed on the very first track scan, enabling the EPC contractor to energize the potline 25 days ahead of the "First Hot Metal" milestone.
| Location | Coastal Smelting & Industrial Corridor, Bahrain |
| Industry | World-Scale Primary Aluminum Smelter Potlines |
| Scale | 1,200m Length; ~190,000 sqm GFA (~26,500 Tons Steel) |
| PTA Crane | Heavy Pot Tending Assembly (PTA) Dynamic Impact Load |
| Rail Tolerance | Span & straightness deviation locked within ≤ ± 1.0 mm |
| Thermal Travel | Accommodates ± 180 mm cyclic coastal thermal drift |
| Ventilation | Continuous high-capacity roof monitors (> 40 ACH) |
| Coating Spec | ISO 12944 C5-M (Marine-Industrial High Fluoride) |
| Connections | 100% Pre-Drilled Bolted Gusset Splices (Zero Hot Work) |
| Schedule Advance | Ready for "First Hot Metal" 25 Days Ahead of Deadline |
Sub-Millimeter PTA Crane Gantry Precision
Machined all heavy crane girder bearing seats on CNC floor-type milling centers, holding continuous track elevation and span tolerances within ± 1.0mm to completely prevent high-speed crane wheel wear and binding.
Thermal-Expansion Sliding Relief Joints
Integrated low-friction PTFE sliding shoe bearings and slotted bolted splices across building sections, releasing ± 180mm of cumulative summer-to-winter thermal expansion with zero frame racking.
High-Airflow Natural Ventilation Roof Monitors
Fabricated continuous aerodynamic ridge ventilators across the entire 1,200m roofline, discharging immense radiant heat from reduction cells without external power.
C5-M Marine-Fluoride Resistant Coating
Grit-blasted to Sa 2.5 with heavy-build epoxy micaceous iron and polyurethane topcoats, resisting scorching sun, maritime salt fog, and acidic fluoride dust for over 25 years.
Turning Site Challenges into Engineered Certainty
Proven technical interventions to keep your project on spec, on budget, and on schedule
In a 1,200m building, +50°C sun causes hundreds of millimeters of thermal growth; binding causes column buckling and crane stalls.
Configured precision Teflon-sliding expansion assemblies with self-lubricating slotted connections every 120m to absorb horizontal creep safely.
PTA cranes operate 24/7 over 1,000°C pots; rail misalignment leads to wheel jamming, stopping cell production and risking solid pot freezing.
Executed 3D CNC profile milling on crane girder joints and pre-mounted adjustable eccentric rail clips, ensuring zero-gap continuous track running.
Coastal Arabian Gulf combines extreme maritime salt air with abrasive alumina dust and hot fluorides, destroying standard steel coatings in months.
Formulated a C5-M high-build epoxy zinc-rich system topped with fluorocarbon sealers, verified under 4,000-hour accelerated cyclic salt-spray tests.
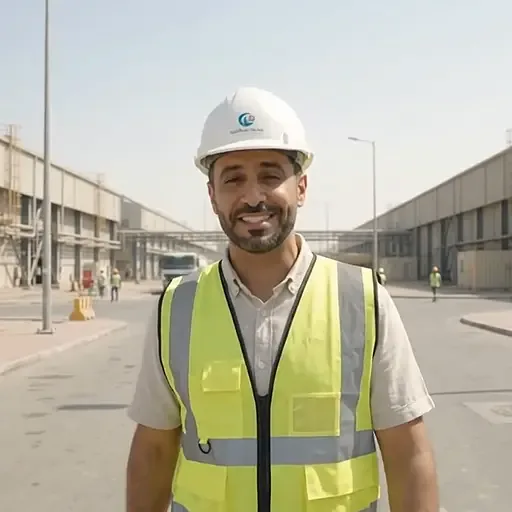
Building a 1.2-kilometer aluminum smelting potline leaves no room for hesitation. Standing at one end, you literally can't see the exit. Under Bahrain’s brutal +50°C summer sun, the massive steelwork expands by hundreds of millimeters. We were terrified of two things: expansion joints binding and twisting the columns, and crane rail misalignment aloft. The multi-million-dollar Pot Tending Assemblies (PTAs) run 24/7 above hundreds of pots boiling with molten aluminum at nearly 1,000°C. If a crane binds or derails aloft because of a warped girder, pots freeze solid, and that is a catastrophic, unrecoverable loss.
Our third-party inspectors grilled Shijie on their thermal expansion design and girder machining tolerances. But the day the first run of crane girders was installed, our total-station laser survey showed the rail span and elevation were held within 1 millimeter down the entire line. When we took the PTA crane on its first full-length test run, the operator came over the radio and said: 'Smooth as ice—zero drag, zero track gnawing.' Across more than 26,000 tons of structural steel, our rigging crew never touched a cutting torch or reamed a single hole aloft. Reaching the 'First Hot Metal' milestone 25 days ahead of schedule saved millions in commercial output. Shijie's precision is world-class.
Products Used in Project
Similar Projects
To be confirmed
Why Global Contractors Choose SynJect
Predictable delivery, certified compliance, and direct engineering support for zero-risk execution
Pre-assembled in our factory and 3D-nested for containers to cut ocean freight and site delays
Fabricated strictly to CE EN 1090-1, AISC, and ISO 9001 / 14001 / 45001 with full NDT traceability
Work directly with senior structural engineers from Tekla 3D modeling to on-site erection
Frequently Asked Questions
To be confirmed
To be confirmed
To be confirmed
To be confirmed
To be confirmed
To be confirmed
Get Your 24-Hour BOQ and Cost Plan
See how much steel tonnage and ocean freight you can save before fabrication begins
Steel Weight Savings
1:1 Tekla 3D modeling optimizes beam-column ratios to eliminate redundant material costs.
Zero-Clash Code Verification
Checked against EN 1090 and local wind/seismic loads.
Engineer-to-Engineer Review
Verified by our lead engineers—Zero pushy sales calls, Just actionable data and factory price.
CE EN 1090-1•ISO 9001•ISO 14001•ISO 45001
Lead Engineers Online
🔒 100% Private and Secure, No Spam