Home / Solutions / Industrial Steel Buildings / Petrochemical Equipment Installation Steel Structures

Heavy-Duty Manufacturing.

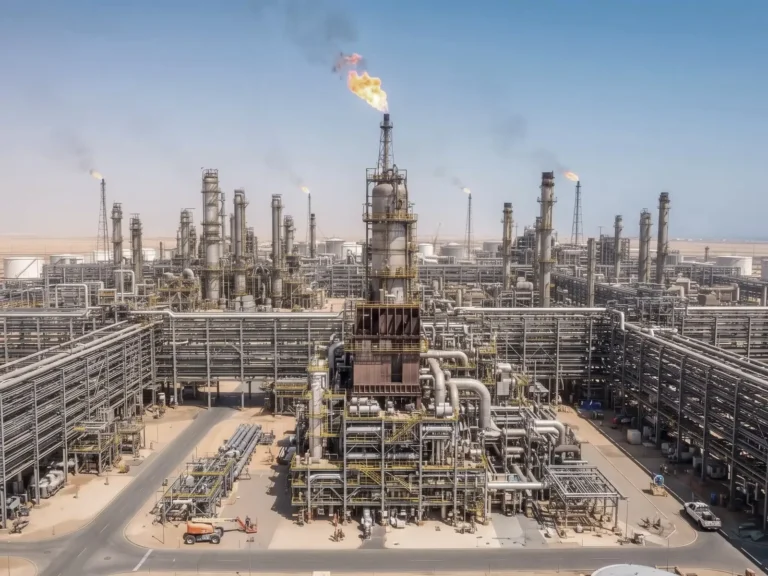
Petrochemical Equipment Installation Steel Structures

Steel structures for petrochemical and energy plants: pipe racks and process frameworks with heavy box columns, equipment supports, substation and transmission steelwork. Critical full-penetration welds are UT or MT tested and the steel is coated to ISO 12944 C4 or C5 or hot-dip galvanised where specified.

What Petrochemical Sites Demand From Structural Steel

Corrosive atmospheres, heavy piping and strict plant standards leave no room for improvised steelwork.

THE CHALLENGE

Pipe racks carrying heavy, hot lines

SJ ENGINEERED SOLUTION

Pipe racks and process frameworks with heavy box columns and full-penetration welds, designed to the piping loads and anchor forces your stress engineer issues; blast-resistant framing is detailed where the plant standard specifies it.

THE CHALLENGE

Corrosion in a chemical or coastal atmosphere

SJ ENGINEERED SOLUTION

ISO 12944 C4 or C5 coating systems (per the plant’s corrosivity category) after Sa 2.5 blasting with dry film thickness recorded, or hot-dip galvanising for towers, gantries and substation steel, as the plant standard names.

THE CHALLENGE

Every weld needs a record

SJ ENGINEERED SOLUTION

Critical full-penetration welds are made to qualified procedures and 100% UT or MT tested, with a report per member; mill certificates are traced to heat number so the QA/QC file is complete before shipment.

THE CHALLENGE

Ancillary steel scattered across the site

SJ ENGINEERED SOLUTION

Transmission and telecom towers, substation gantries, equipment supports and wind farm ancillary steel are fabricated in the same shop, galvanised and shipped in bolted sections marked to the erection drawings.

How Your Project Is Built

Three phases from the first drawing to handover. Move over a phase to see what happens in it and what you receive at the end of it.

PHASE 01 / PRE-CONSTRUCTION

Engineering & Foundation

The structure is sized in a 3D BIM model before any steel is cut. While members are fabricated in the factory, earthworks and independent foundations are poured on site in parallel from the anchor bolt templates we ship first.

PHASE 02 / CONSTRUCTION

Fabrication & Erection

Columns, beams and trusses are CNC-cut, welded, tested and trial-assembled in the yard, then shipped in erection sequence. On site the frame is bolted from marked members with the erection drawings and our remote or on-site guidance.

PHASE 03 / COMPLETION

Envelope & Handover

Cladding, insulation, openings and rainwater goods close the building; dimensional and coating records are handed over with the as-built drawings and the certificate package.

CERTIFICATIONS & COMPLIANCE

Certifications & Compliance

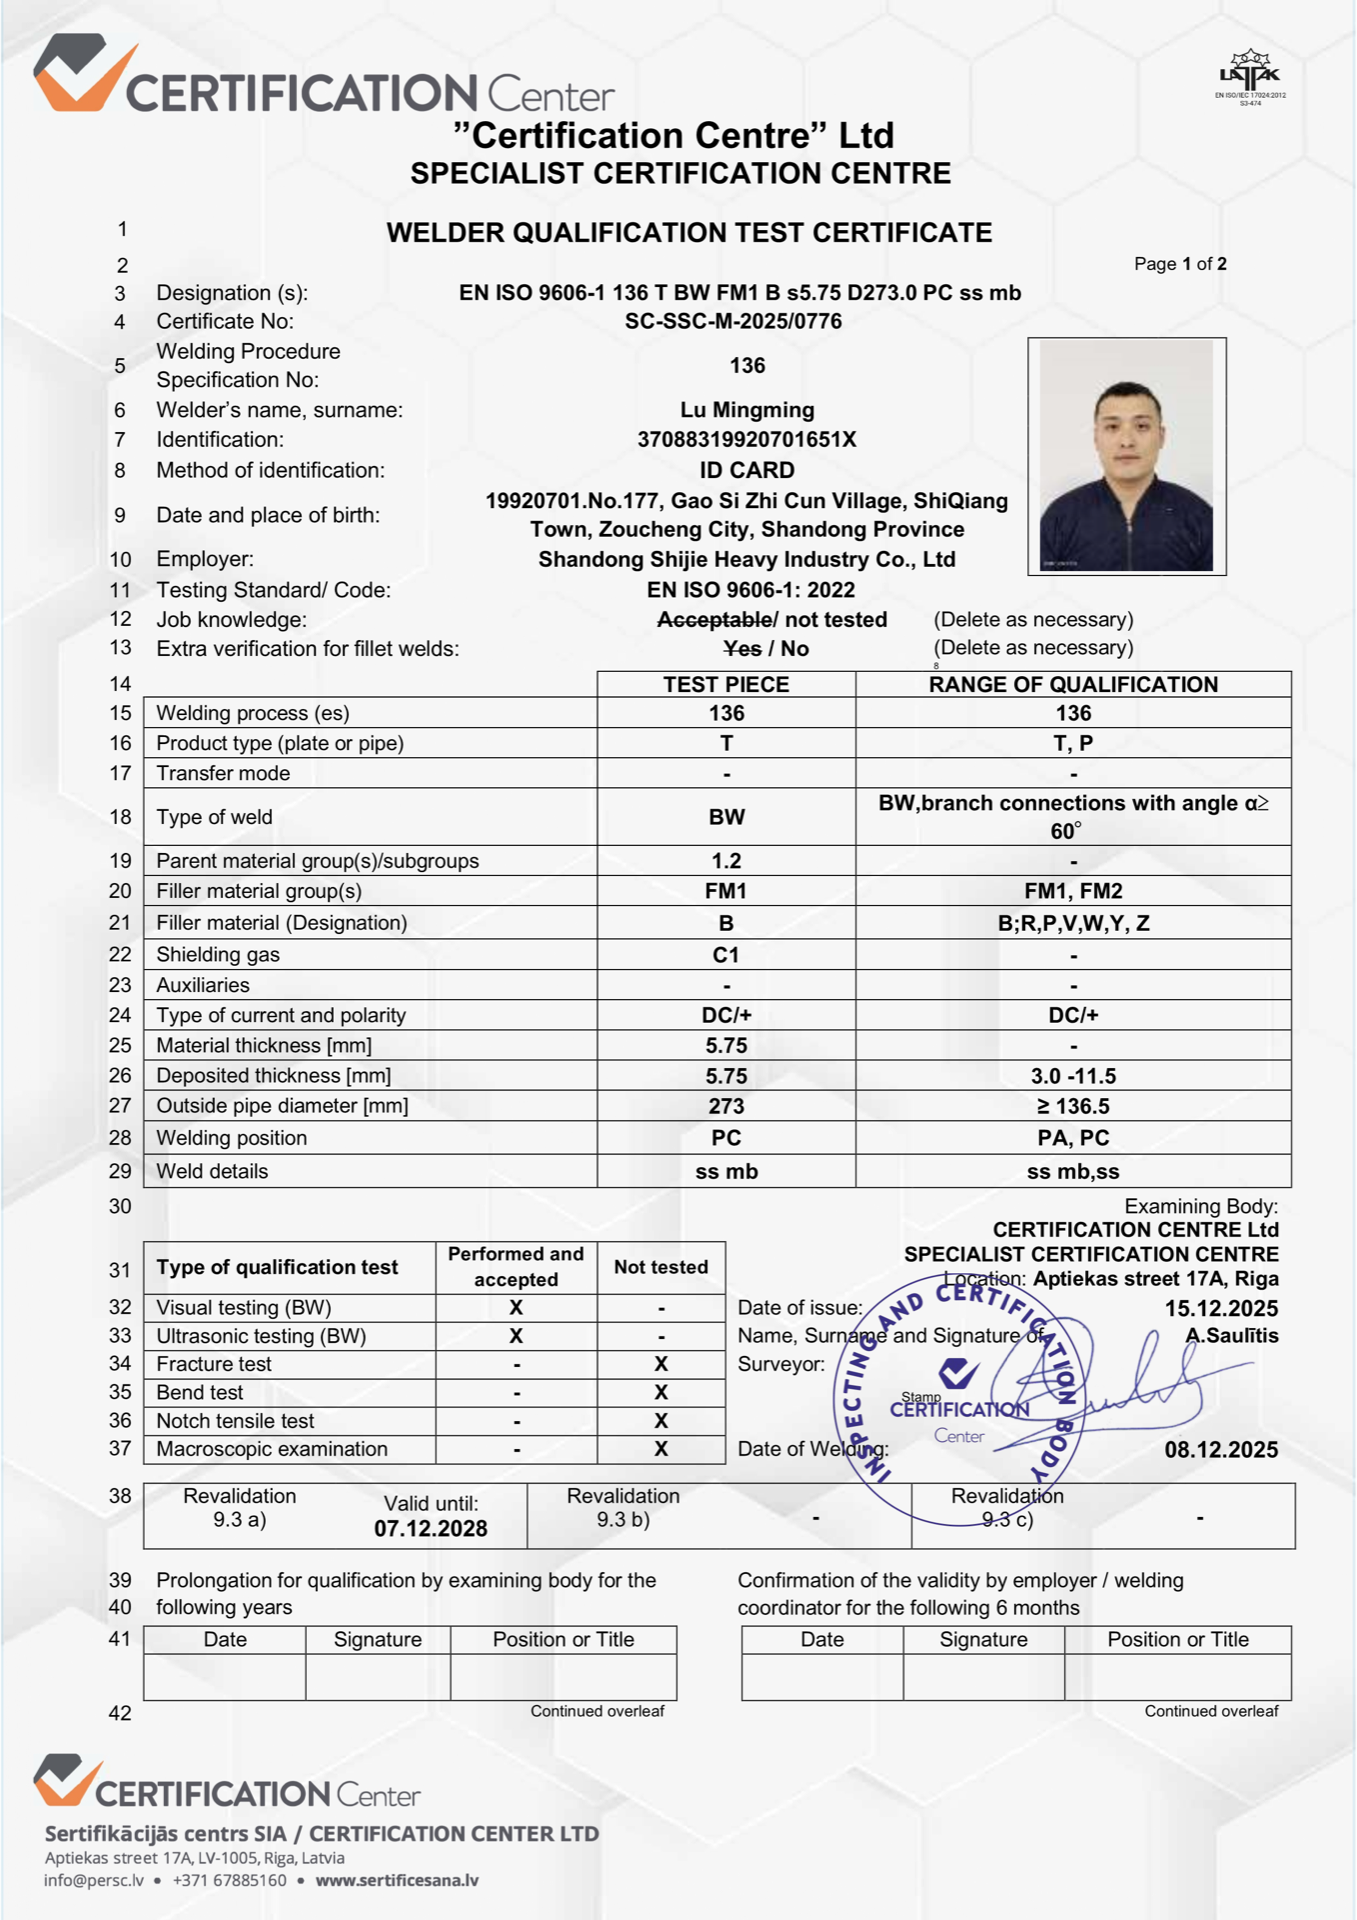
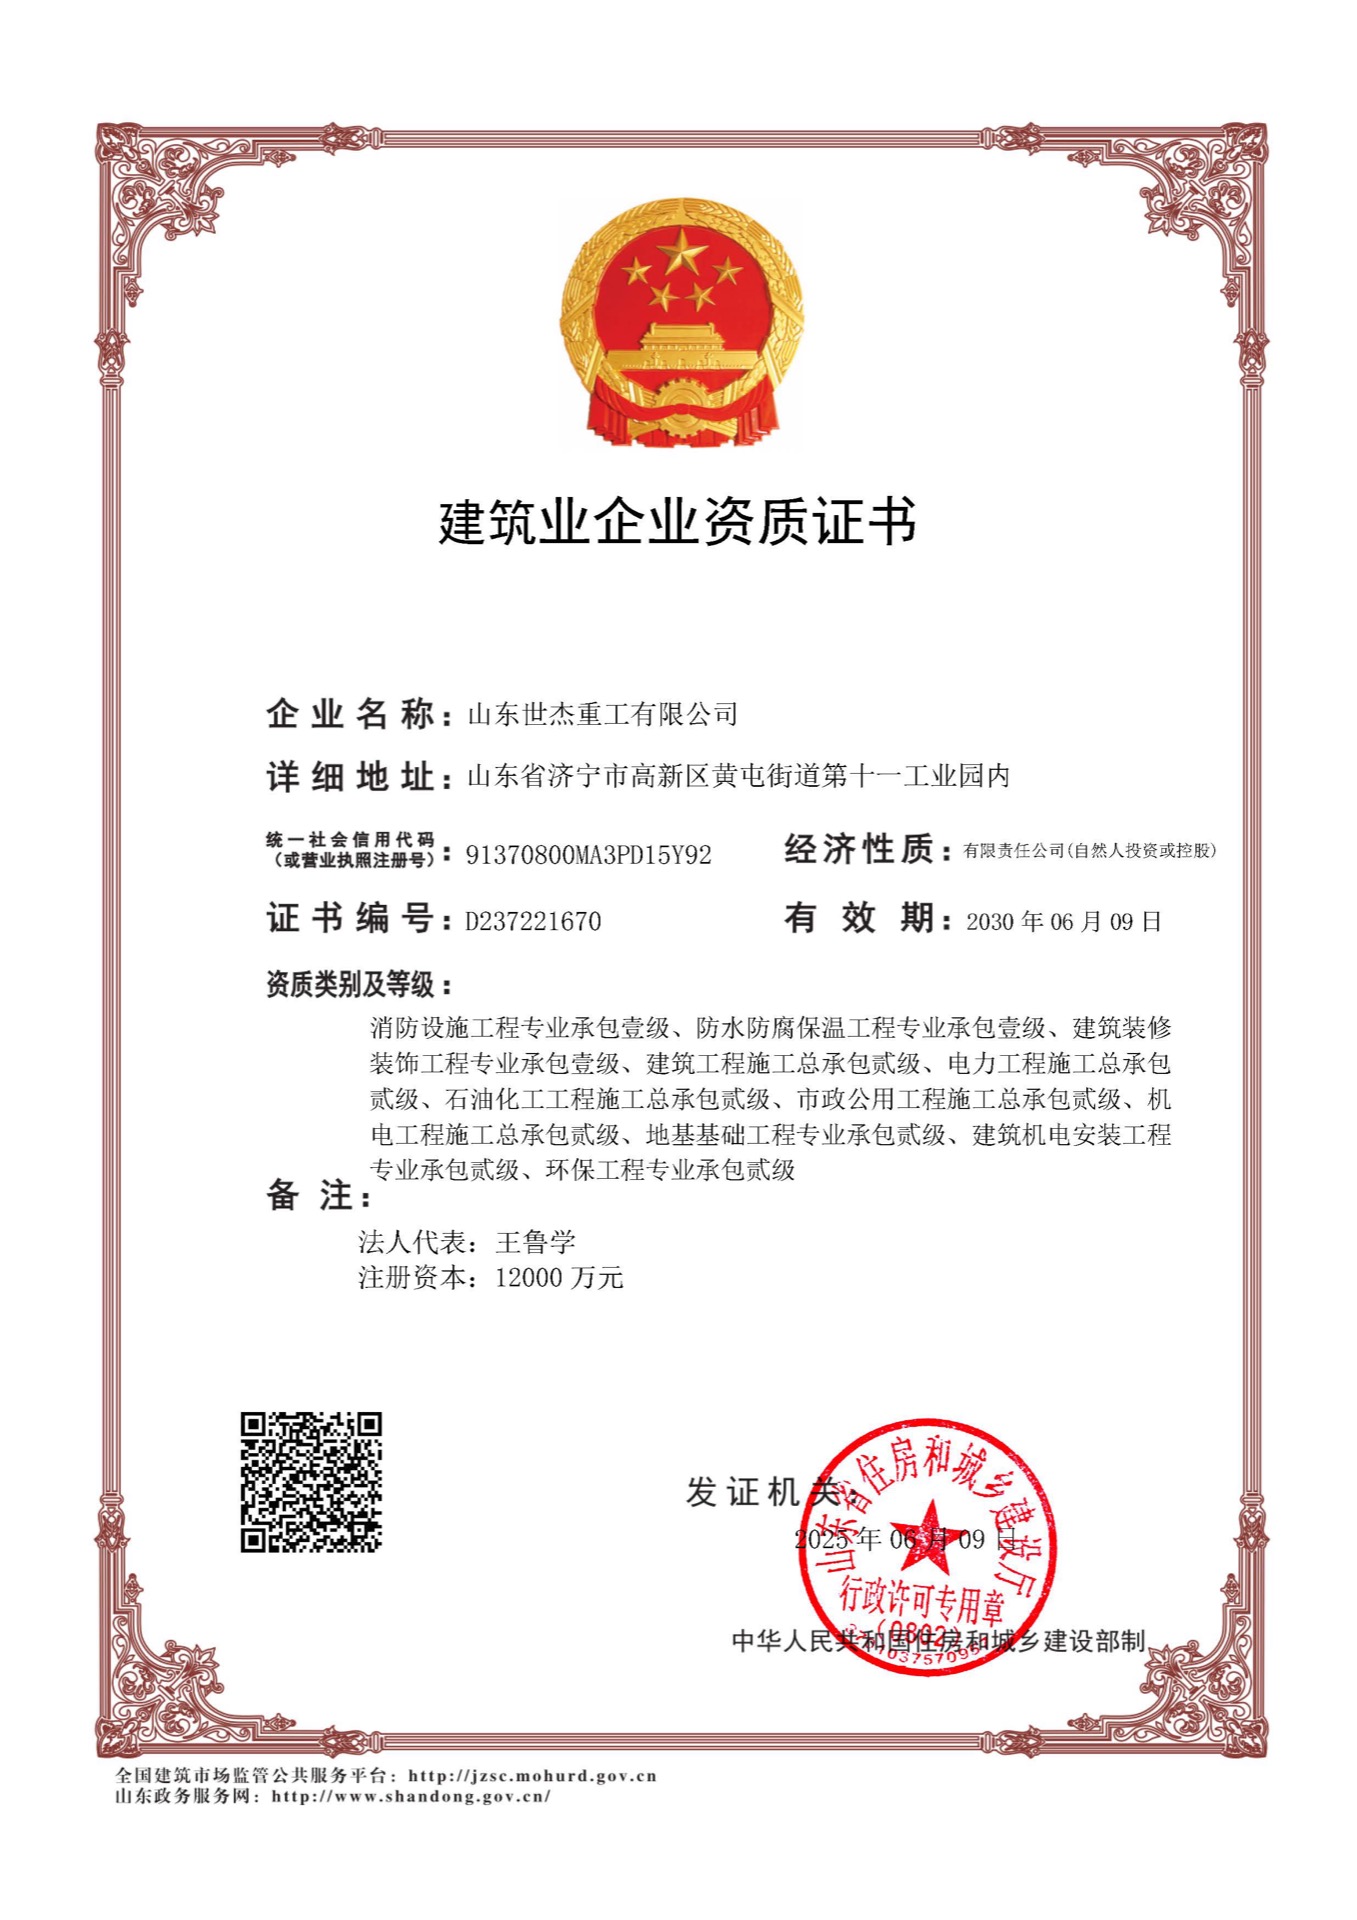
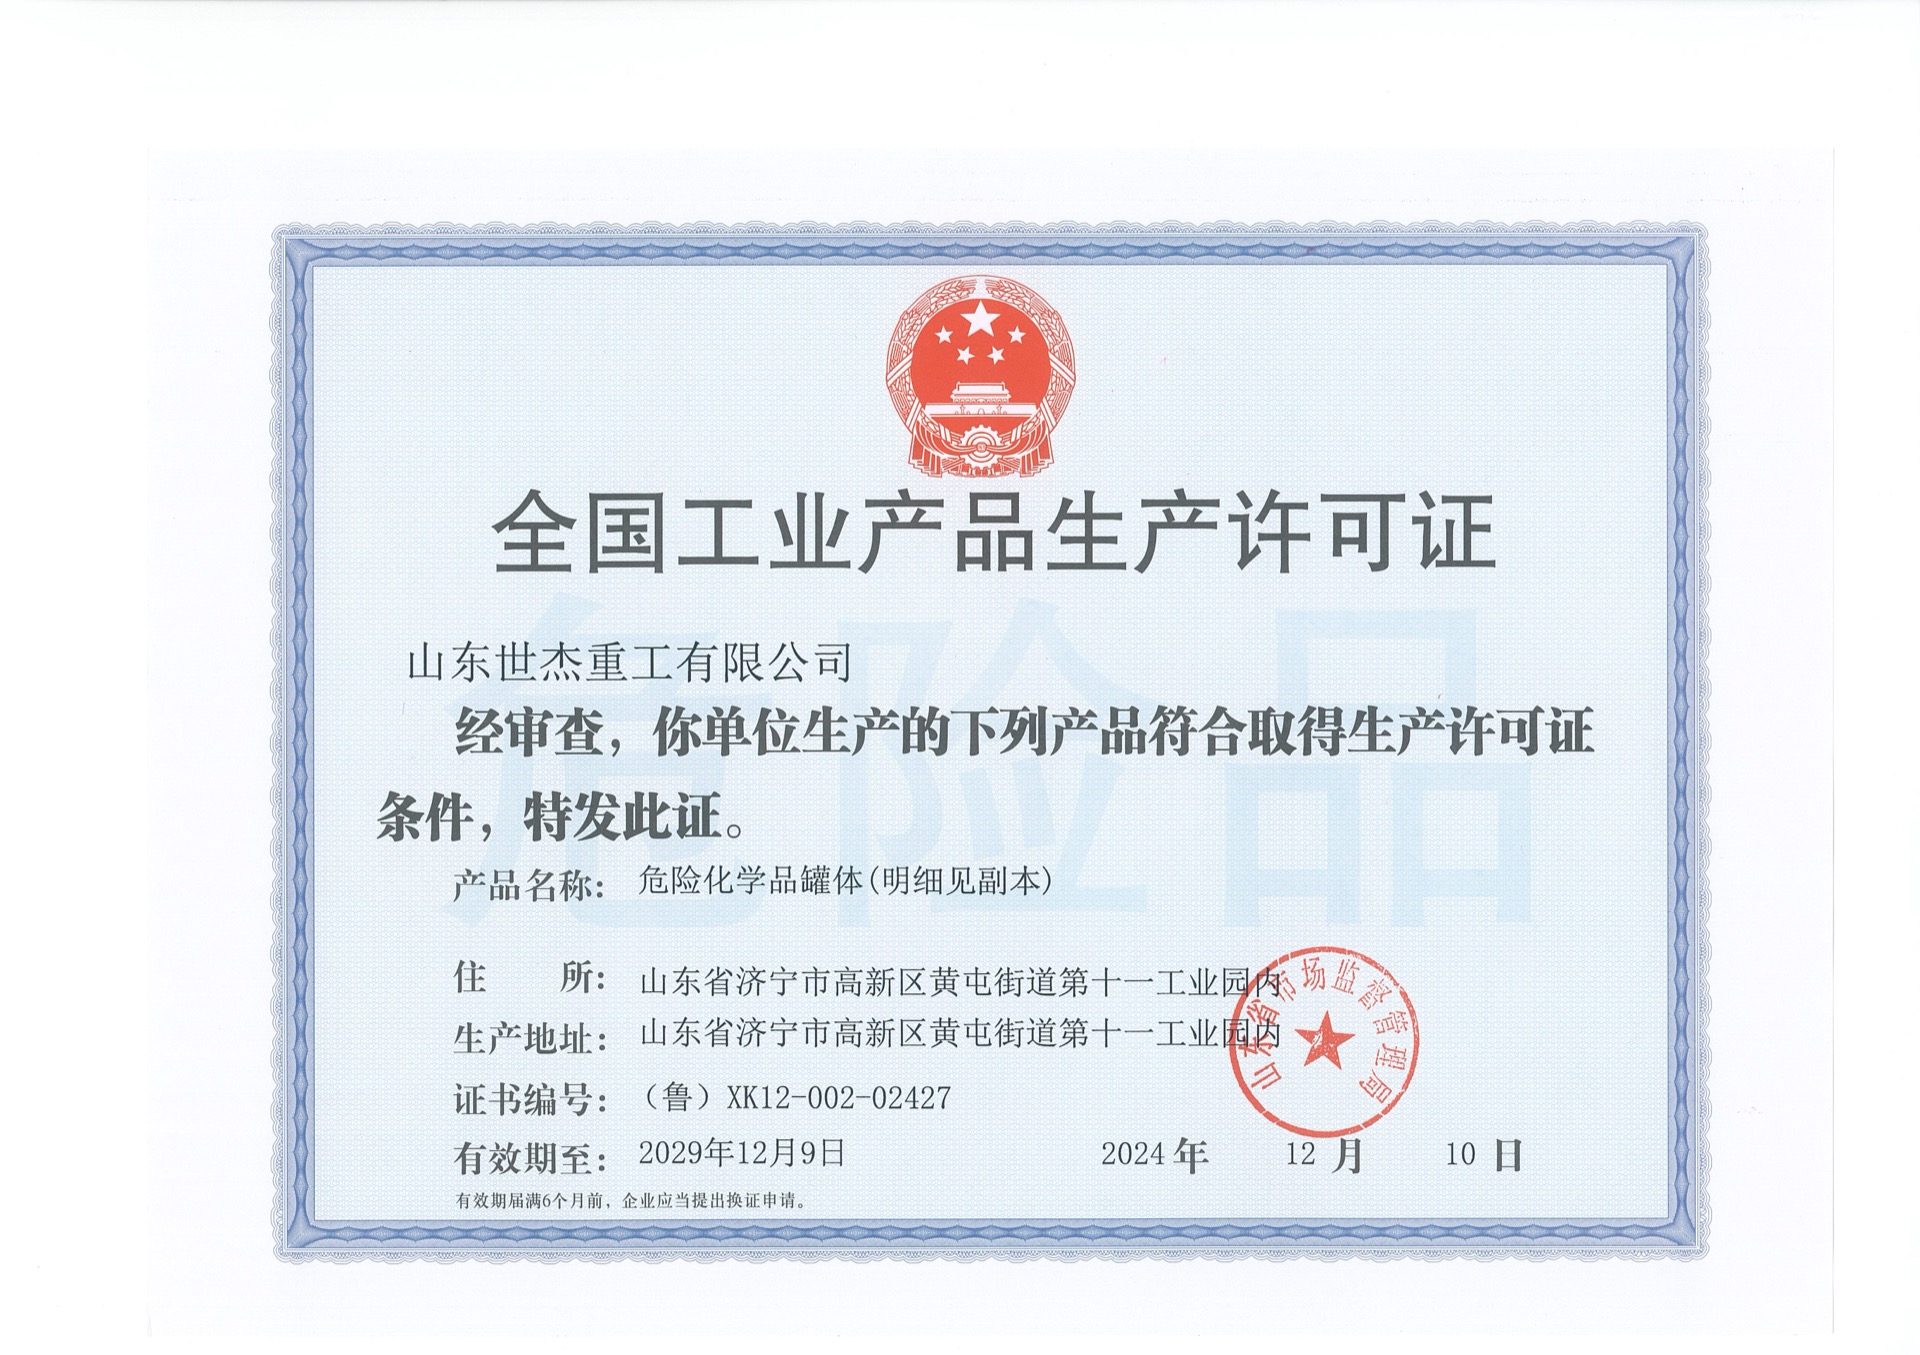
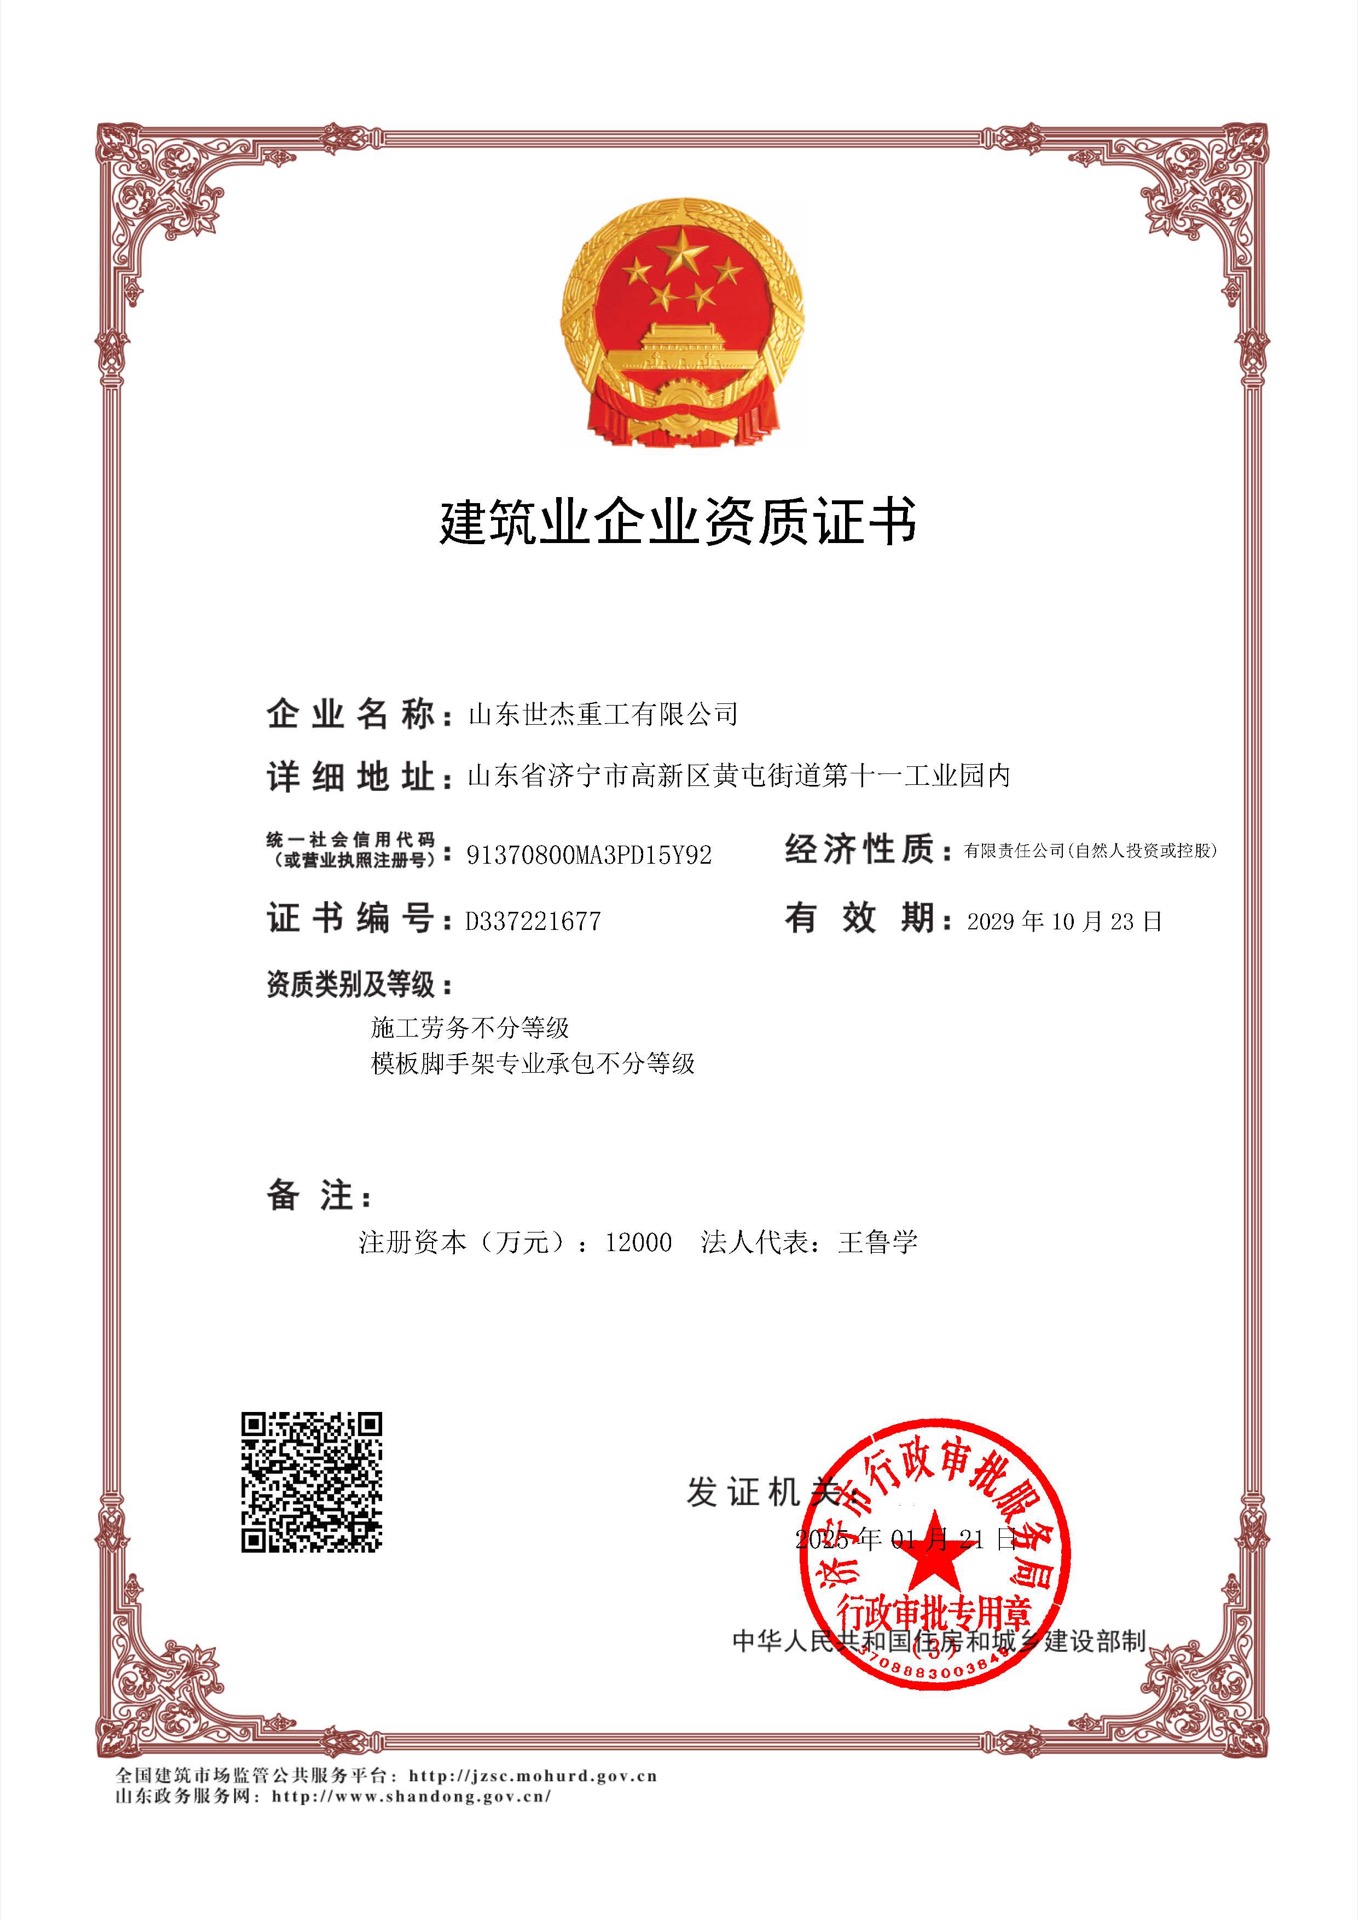
Every shipment leaves with the documents an auditor asks for. Scroll the row and open any certificate at full size.

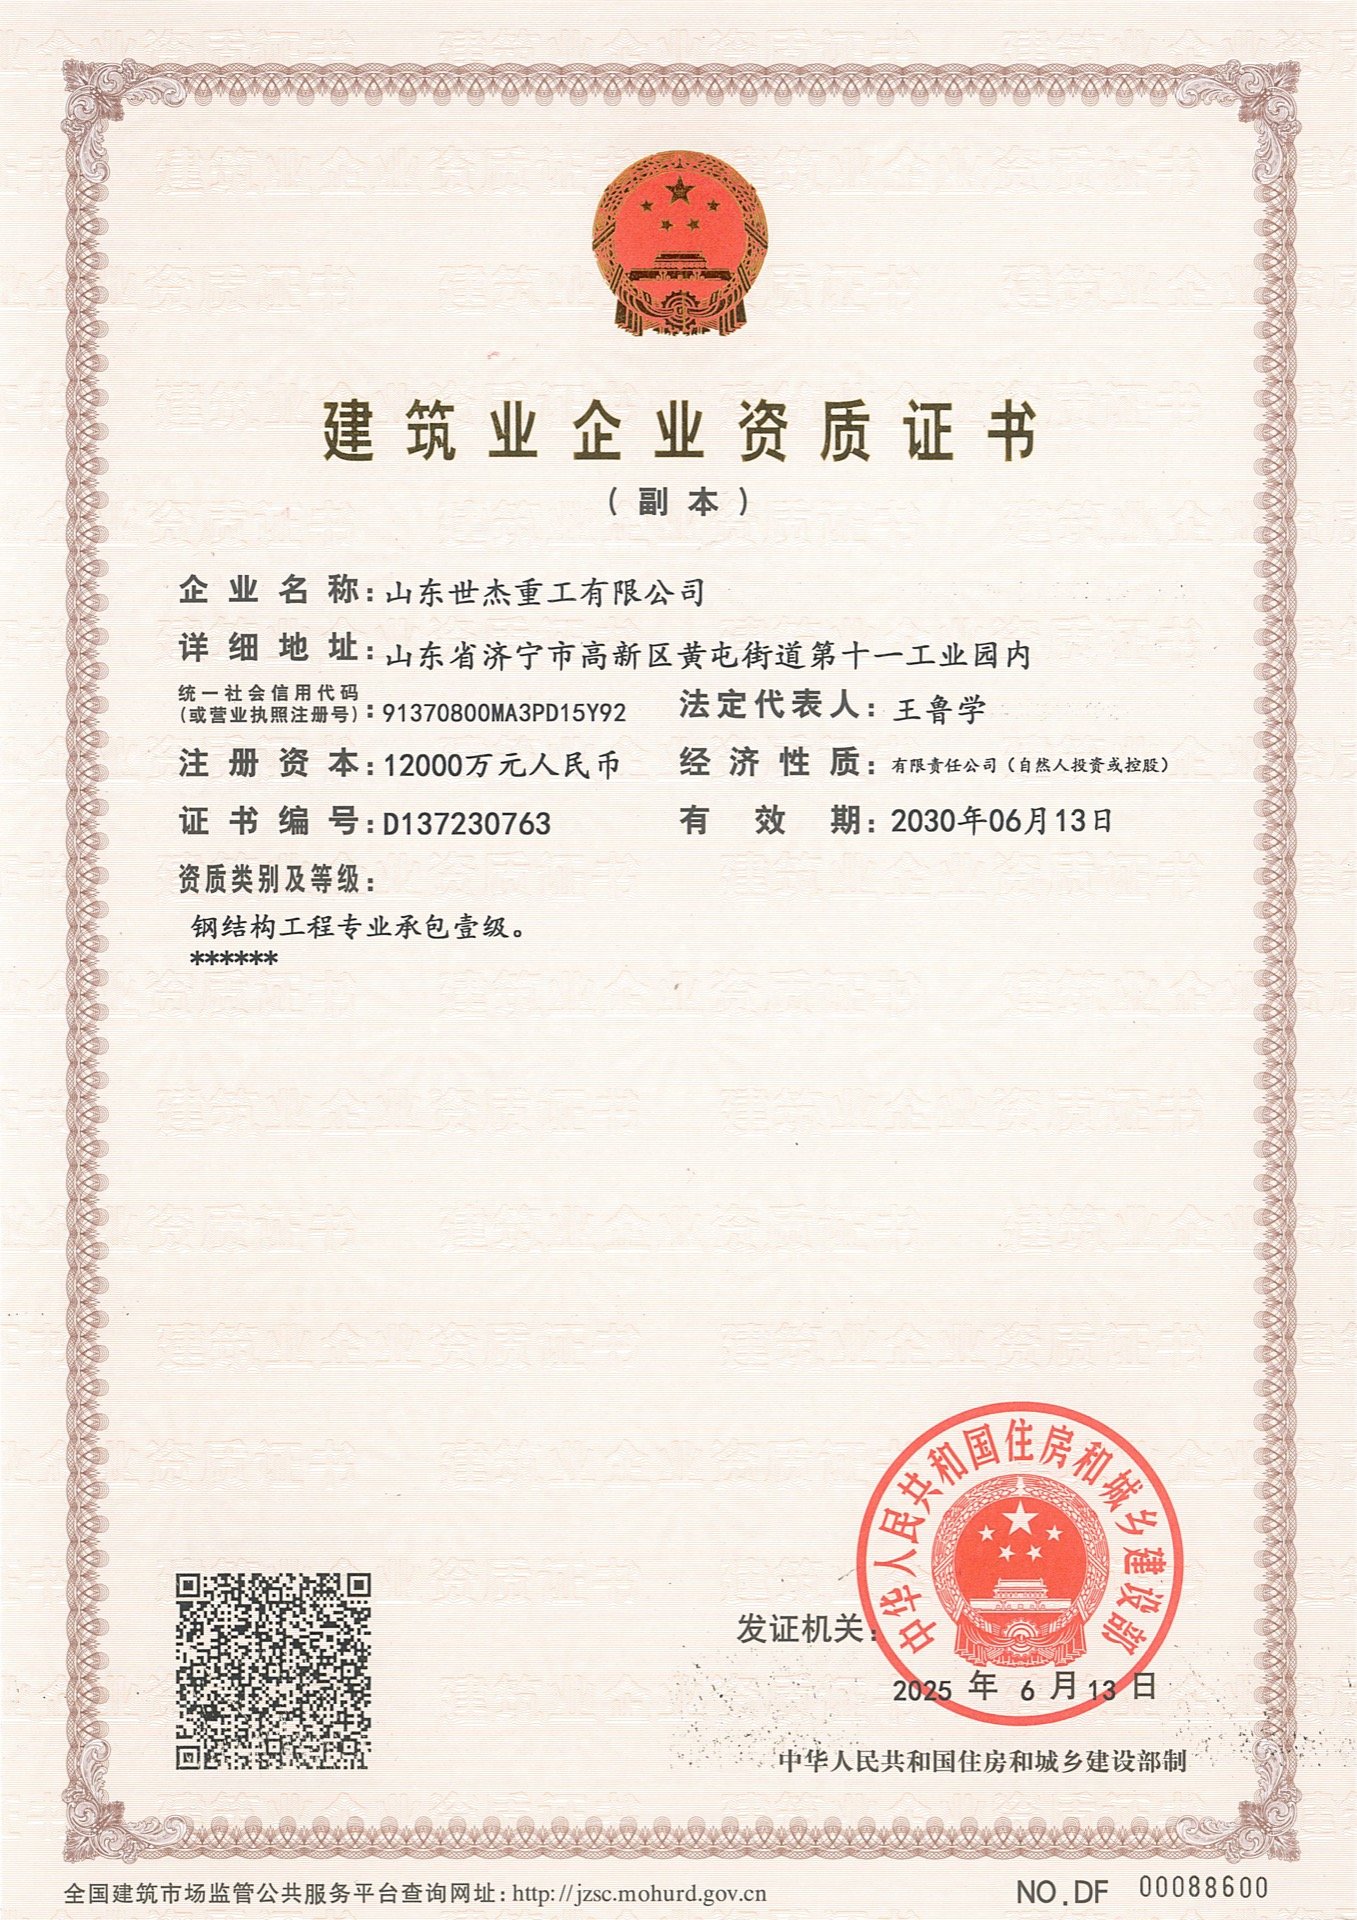
China Steel Structure Manufacturing Grade I

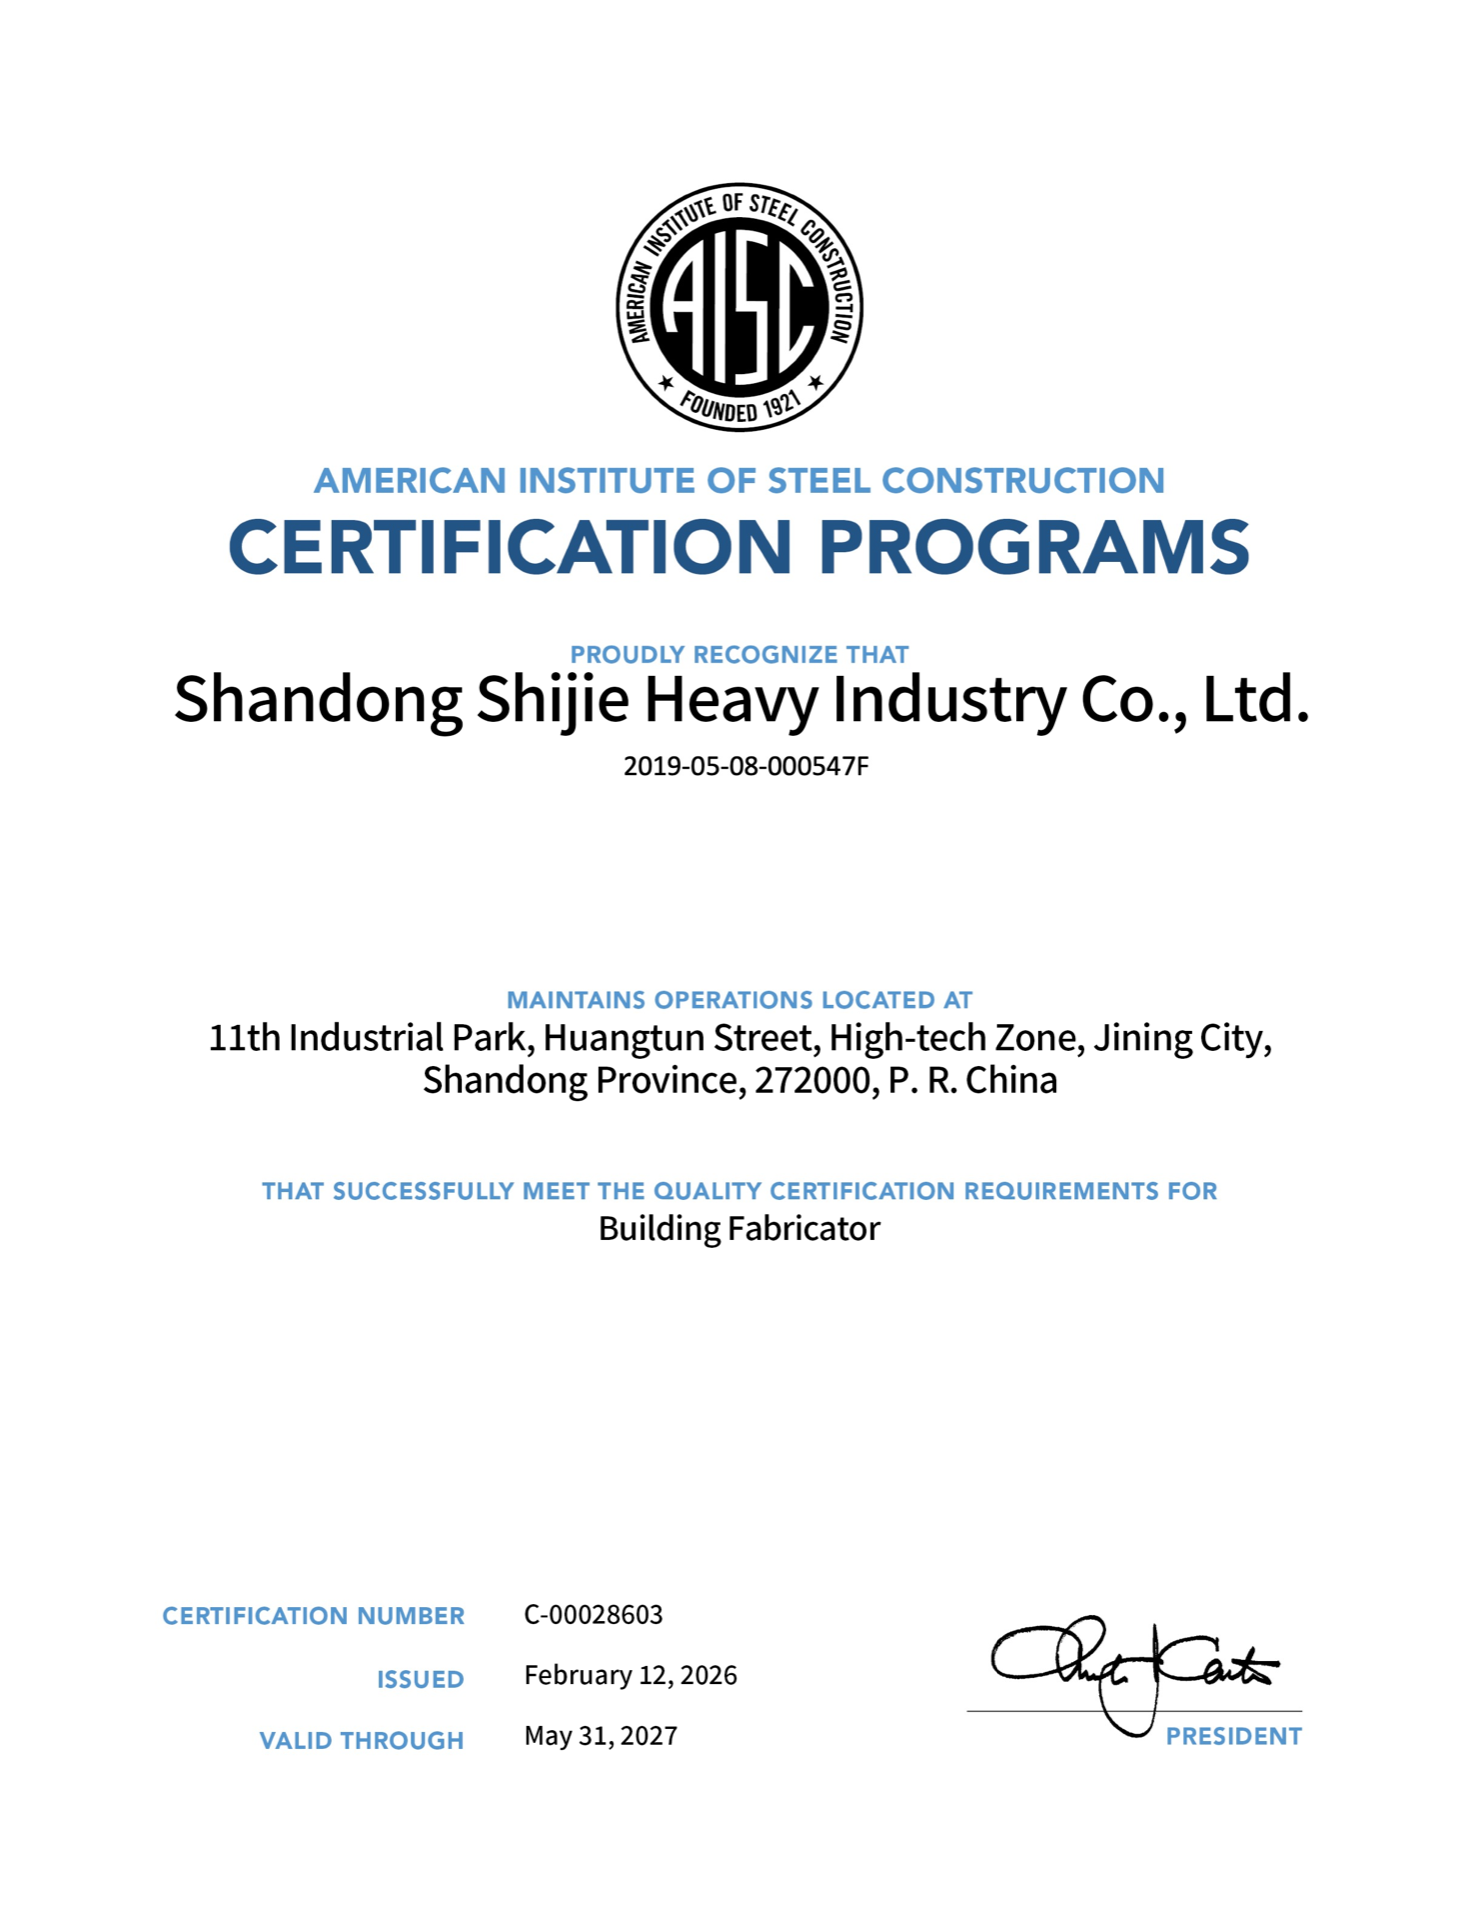
AISC Certification

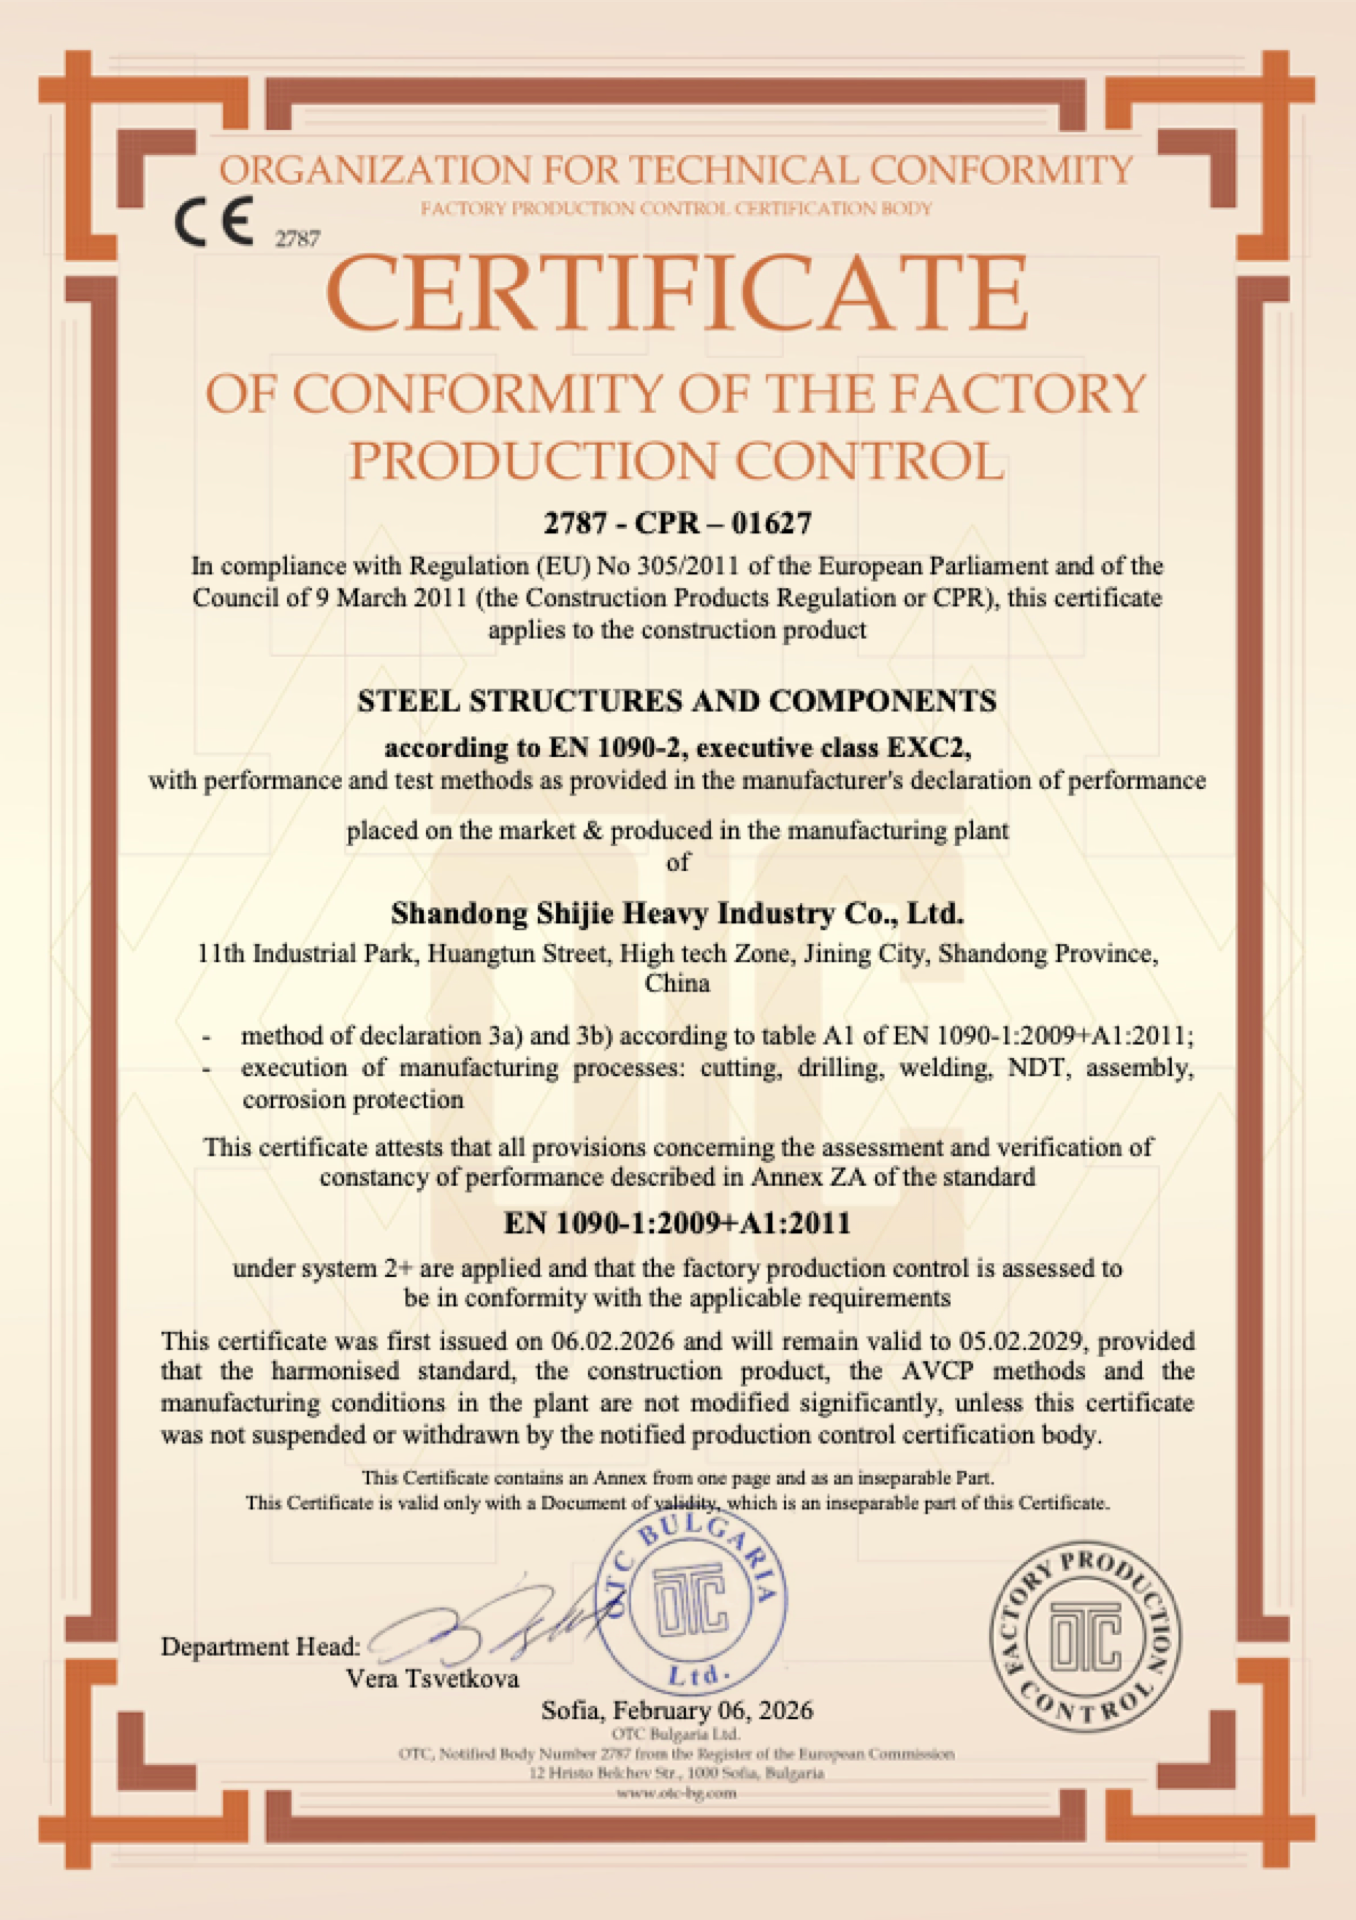
CE Marking – EN 1090-2 (CPR 01627)

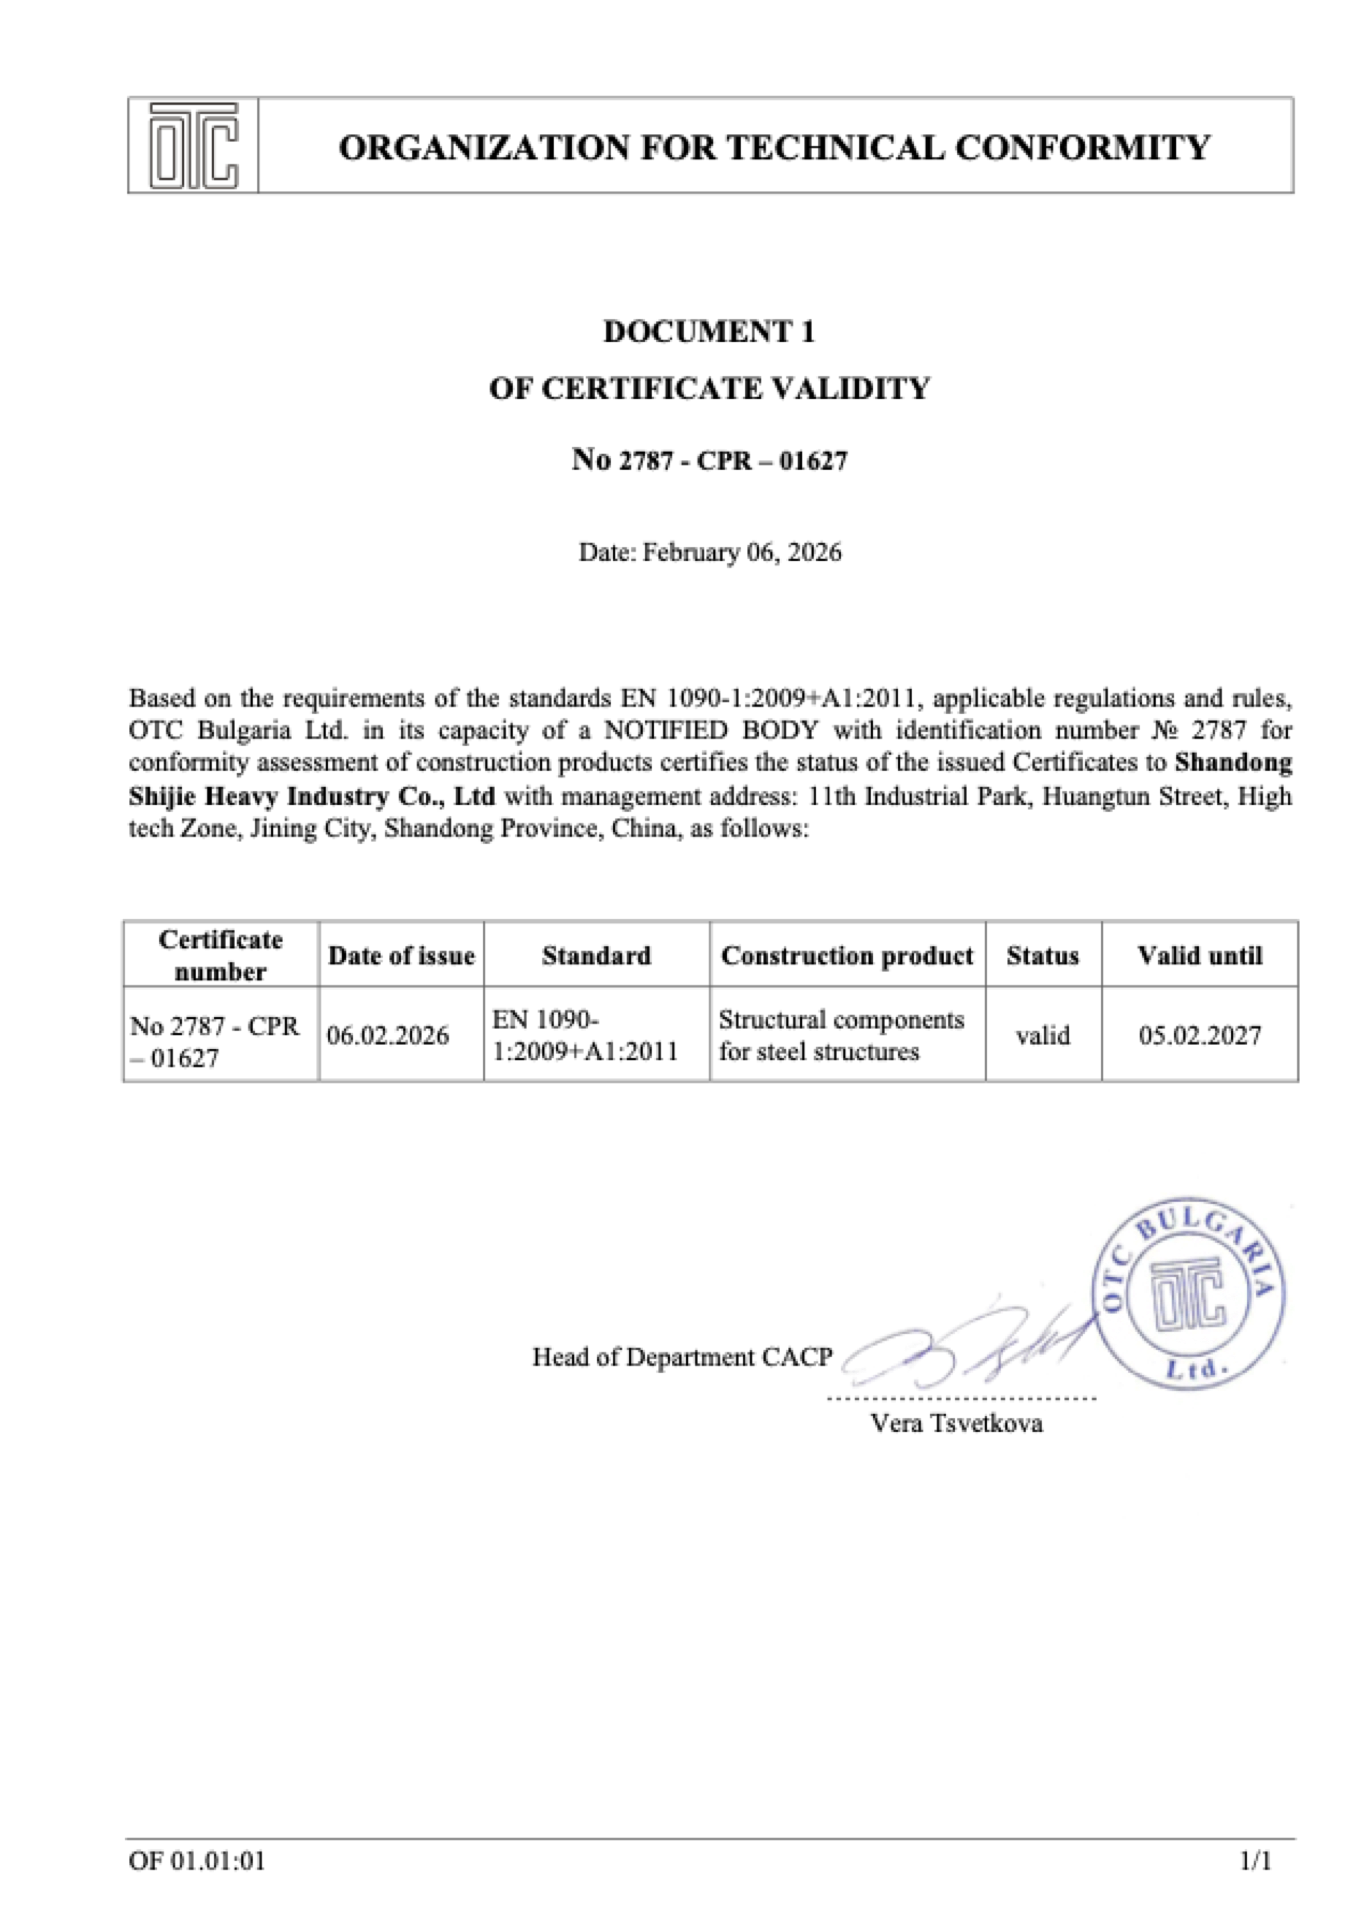
OTC Document of Validity

International Welder Certification

Enterprise Qualifications Portfolio

DG Packaging Certificate

Labor & Scaffolding Contracting

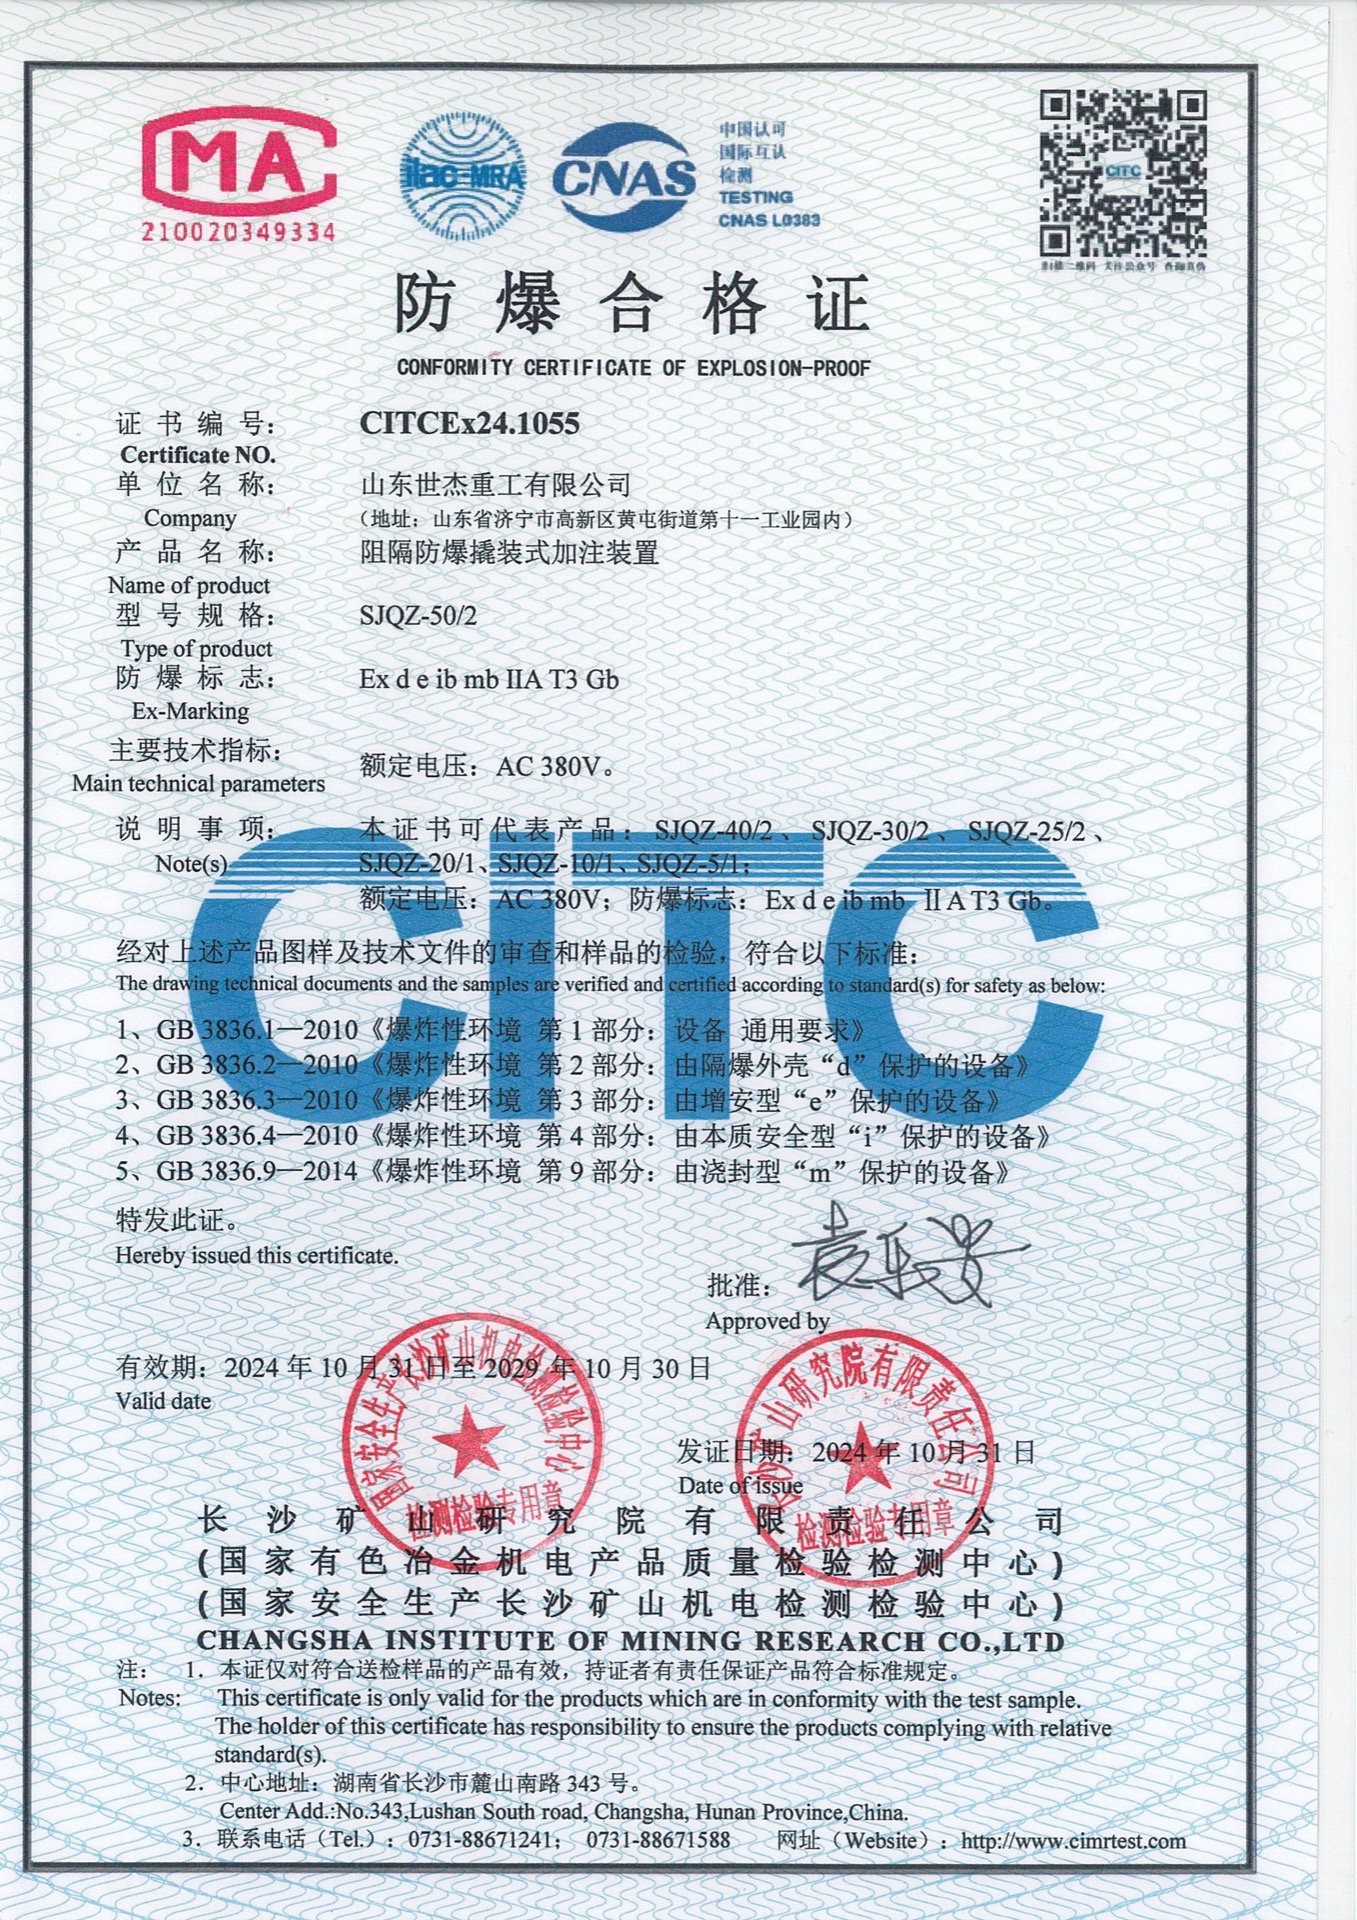
Explosion-Proof Certificate

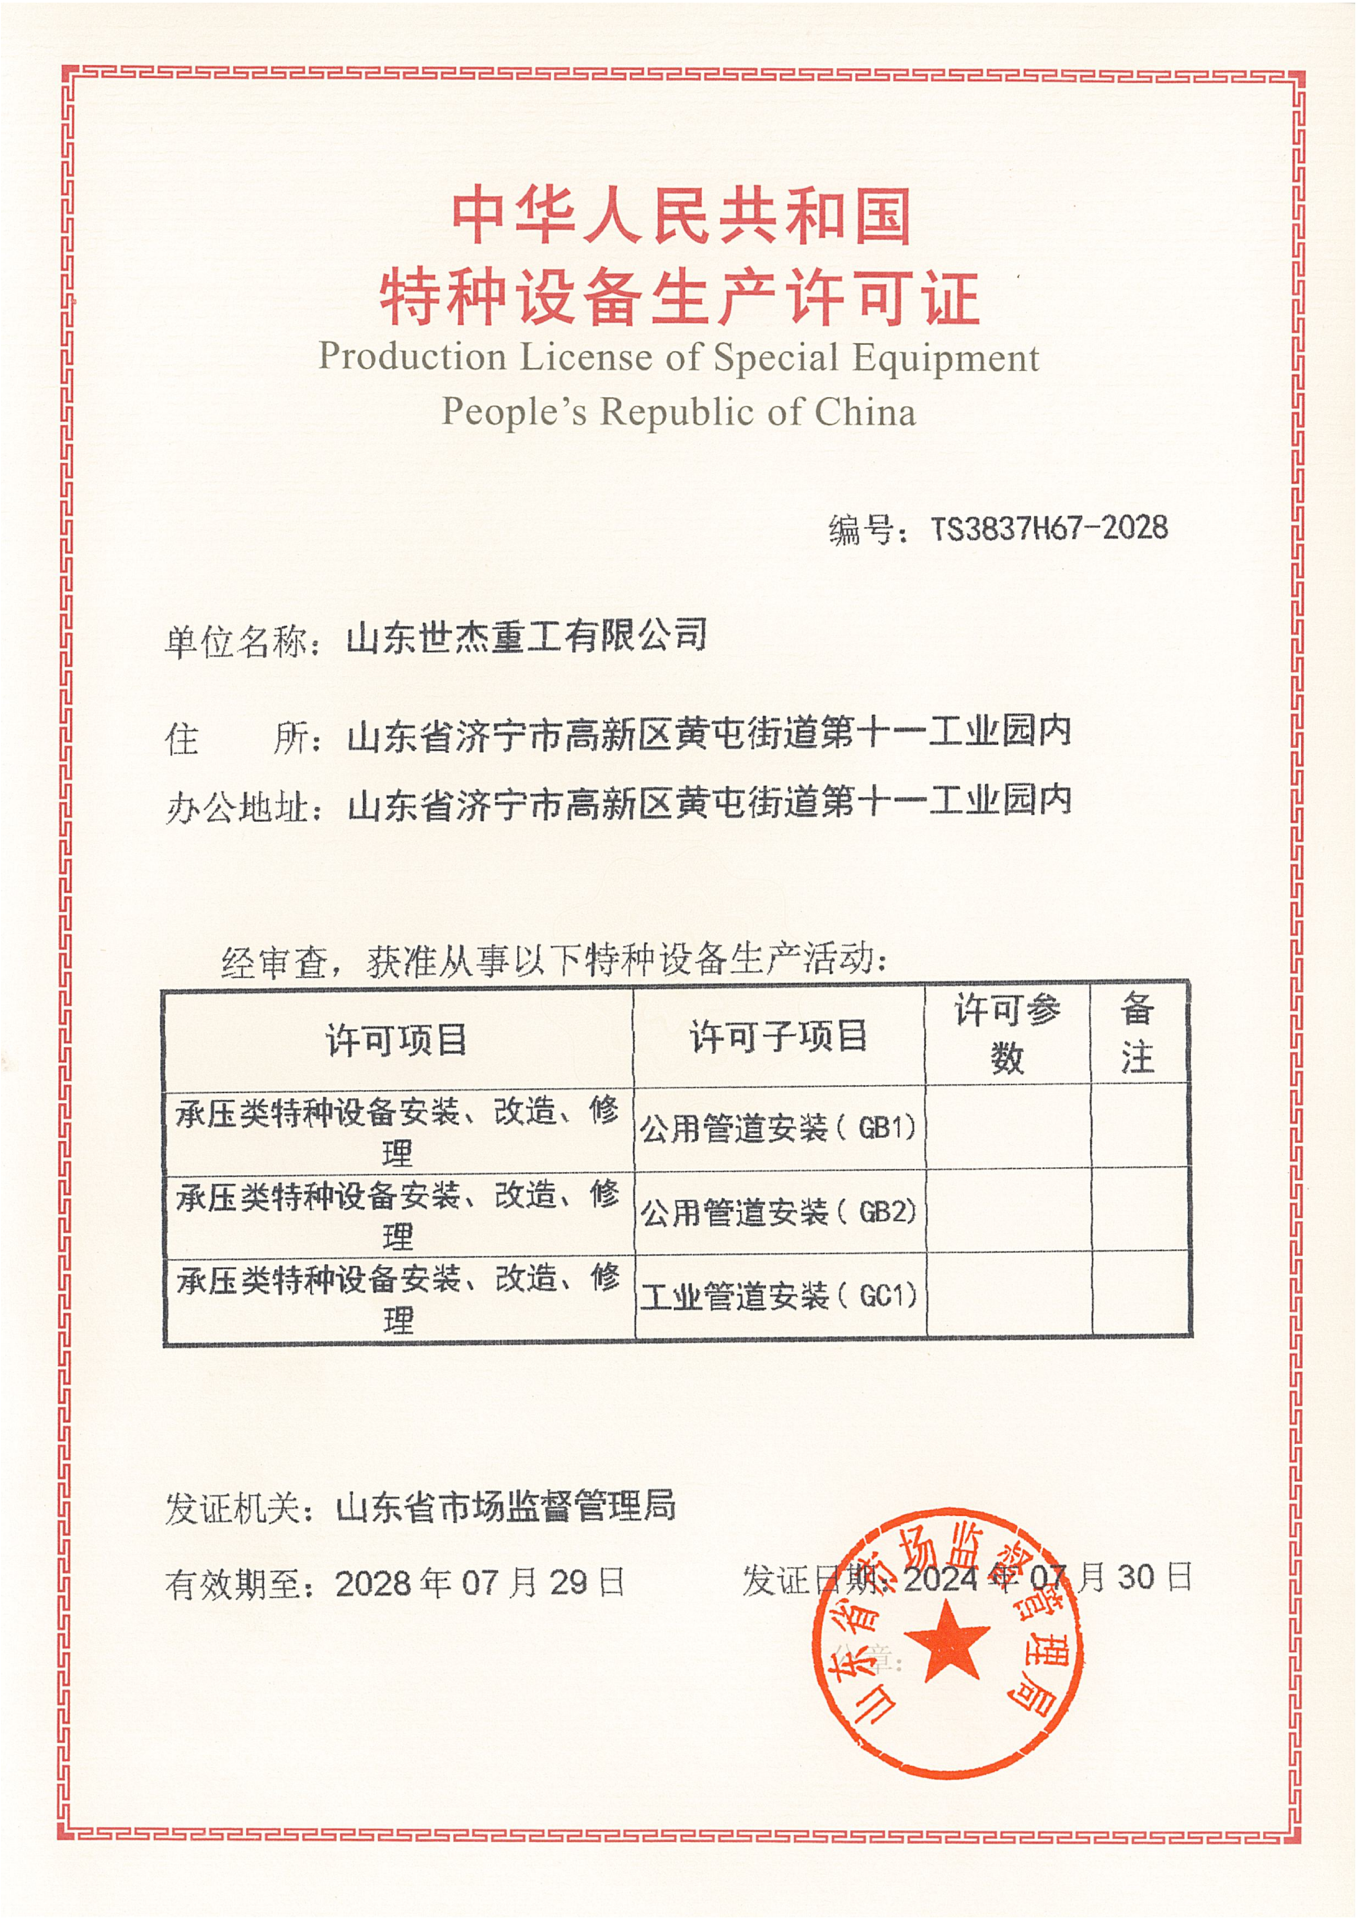
Industrial Pipeline Installation GC1

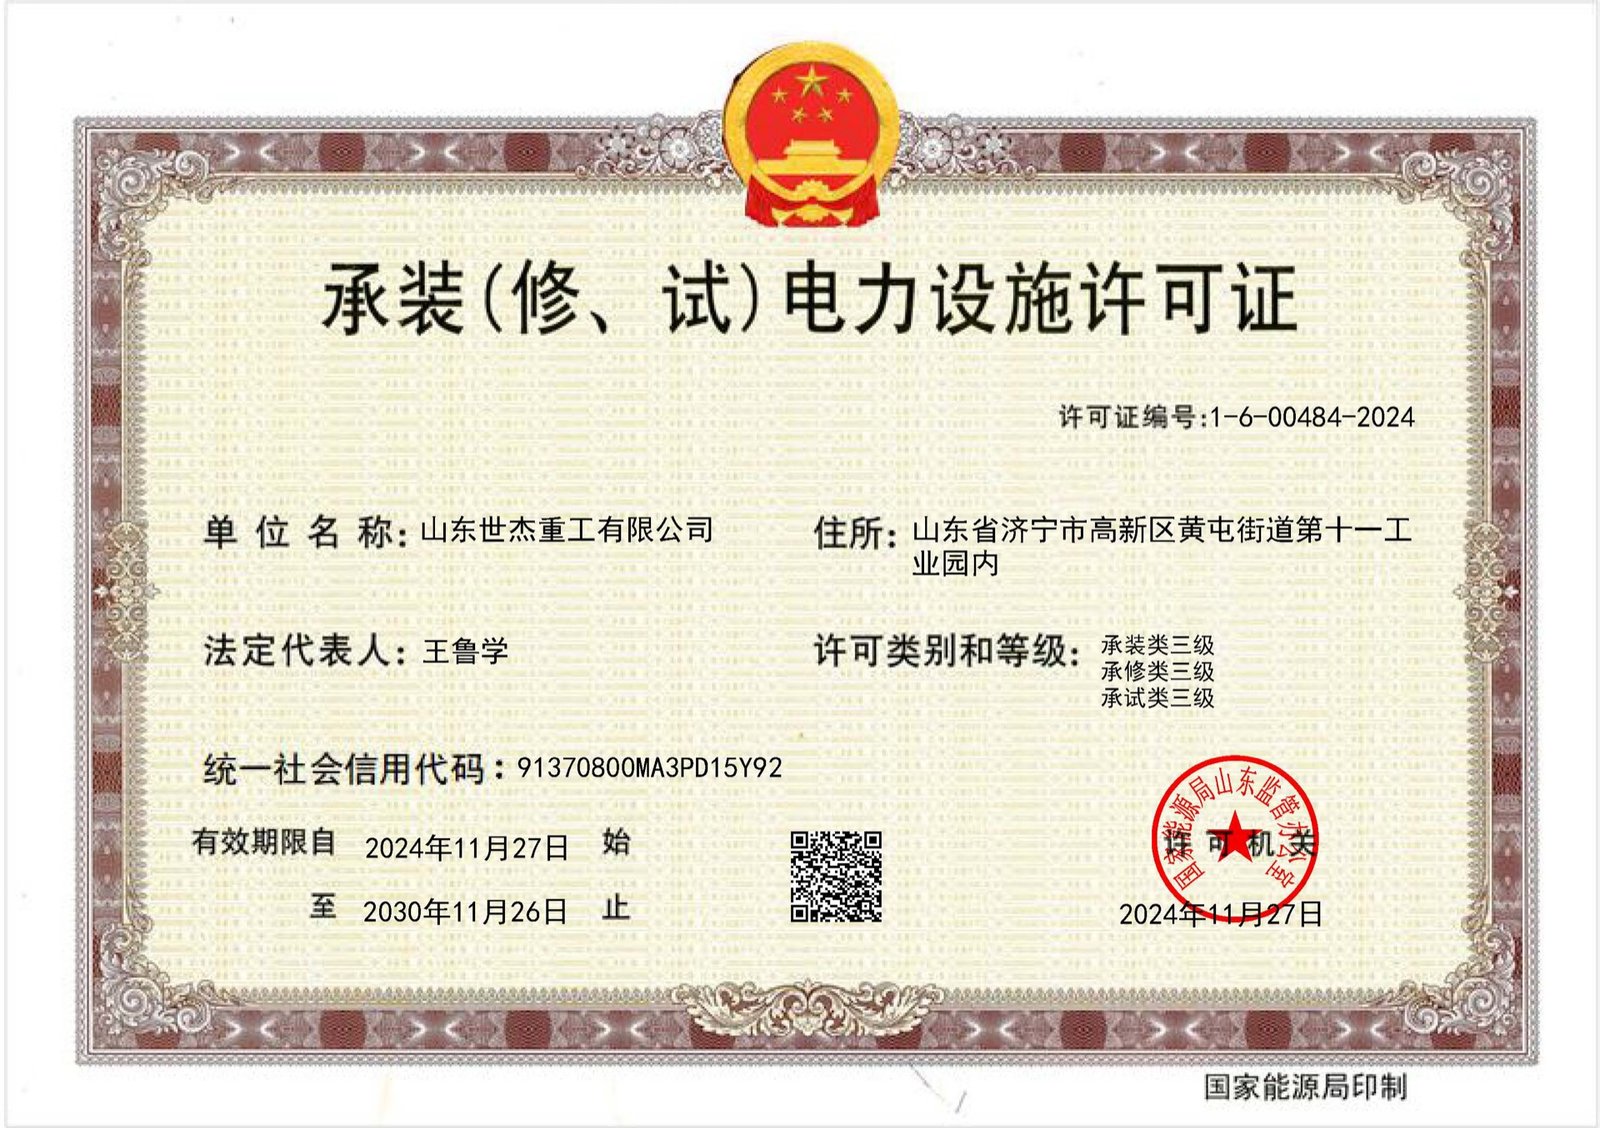
Power Facility License

Technical Parameters

What the steelwork is sized from, and what is fixed before fabrication.

ParameterWhat it is set from
StructuresPipe racks, process frameworks, equipment supports, towers, substation gantries and ancillary steel to the plant design
Design basisAISC 360 / EN 1993, with the plant standard governing blast, fire and corrosion requirements
LoadsPiping loads and anchor forces from the stress analysis, equipment loads, wind and seismic loads for the site
Corrosion protectionISO 12944 C4 or C5 coating per the plant’s corrosivity category, with DFT records, or hot-dip galvanising to the specified coating mass where specified
Welding and NDTAWS D1.1 / EN ISO 9606 qualified procedures; critical full-penetration welds 100% UT or MT tested
Execution classEN 1090-2 EXC2 (certificate 2787-CPR-01627)
Steel gradesS355 / S460 to EN 10025, ASTM A36 / A992, with EN 10204 type 3.1 mill certificates
Lead time40 to 50 days for a typical single-building portal frame scope: 1–2 weeks to shop drawings for your approval, then 4–5 weeks for fabrication, coating and loading; larger or multi-building projects are phased by building
DocumentationMTRs, WPS/PQR, welder certificates, NDT and DFT reports, erection drawings and the certificate package with every shipment

Recommended Product Systems

The structural systems we fabricate most often for this kind of project. Each opens the product page with sub-systems, parameters and FAQ.

Multi-storey steel buildings from one fabricator: thick-web H and box columns, cruciform columns, steel floor beams, composite decking and stairs for commercial and industrial frames, with embedded parts and anchor bolts shipped ahead of the steel.

Pre-engineered buildings on a steel portal frame, the rigid frame building type of every PEB catalogue: tapered H-section primary frames, cold-formed purlins, bracing and anchor bolts detailed as one system for workshops, warehouses and agricultural halls.

Steel truss structures for long-span roofs: circular pipe trusses, square tube trusses, angle steel trusses and H- or I-beam trusses fabricated as roof truss systems for terminals, stations, industrial halls and exhibition centres.

Building envelope systems quoted with the steel frame: roof and wall cladding, insulation and waterproofing, industrial doors, windows, louvers and ventilators, gutters and downspouts.

Frequently Asked Questions

Do you design the pipe rack or fabricate to our drawings?

Either. Send the piping loads and anchor forces from your stress analysis and we design and detail the rack, or we fabricate to drawings your EPC contractor has already issued.

Where the plant standard specifies it, yes — the framing is detailed to the blast load case your engineer issues, with the welds and connections that case requires.

ISO 12944 C4 or C5 systems (per the plant’s corrosivity category) applied after Sa 2.5 blasting with dry film thickness recorded per member, or hot-dip galvanising for towers and gantries, as the plant standard names.

Yes. Lattice towers in hot-dip galvanised angle steel, substation gantries and equipment supports are fabricated in the same shop and shipped in bolted sections marked to the erection drawings.

Yes — racking, brackets and rails are quoted as a separate line; PV modules and electrical equipment stay with your system integrator. See the Solar PV Mounting Structures product line.

Mill certificates per heat, WPS/PQR, welder certificates, NDT reports with technician level, coating thickness records and the CE and AISC certificate package.

REQUEST A QUOTE

Send Us Your Drawings or BOQ

Tell us the footprint, span, crane capacity and local loads — our engineering team reviews every request and replies with a preliminary assessment.

🔒 100% Private and Secure, No Spam